



Sworznie do tłoczenia stali nierdzewnej: Materiały i opcje powłok
There is no single best material or coating for punch pins used in stainless steel stamping. The right combination depends on the stainless grade and condition, Grubość arkusza, Geometria dziurkarki, Produkcja, Smarowanie, Przebieg, Dostęp, and the failure mode already appearing in production.
A punch substrate provides the bulk toughness, Wytrzymałość ściskająca, and edge support. Heat treatment establishes its usable hardness and fracture resistance. Surface finish affects friction and material pickup. The coating or surface treatment then modifies wear, Ciepło, and sliding behavior. Choosing only one of these elements rarely solves the complete problem.
This guide focuses on punch pins used to pierce or blank stainless steel sheet. It does not assume that the punch itself must be made from stainless steel. Dla szerszych informacji o typach matryc, system-level material selection, Dostęp, Tolerancje, oraz źródła, zobacz Przewodnik po formach wybicia (wnioskowane).
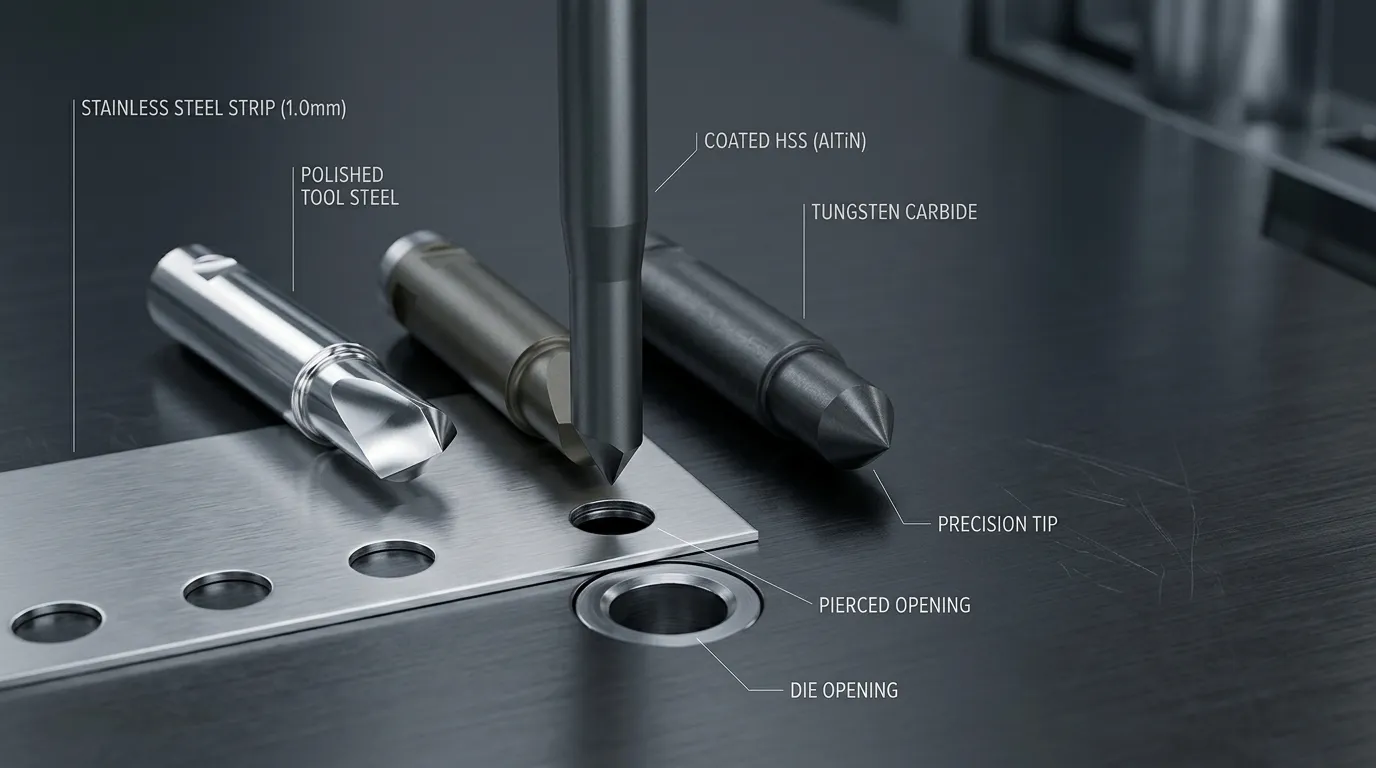
Dlaczego stal nierdzewna zmienia wybór sworzni dziurkackich
Stainless steel is not one uniform work material. Austenitic, ferritic, martensitic, and duplex grades have different mechanical properties and forming behavior. The Przegląd rodzin stali nierdzewnej WorldStainless is useful background, but the tooling decision must go further than identifying the family name.
The supplier or tool engineer should know:
- the exact stainless grade;
- Grubość arkusza;
- temper, Twardość, or tensile condition;
- Stan powierzchni;
- pierced-hole or blank geometry;
- expected production quantity;
- lubrication method or restrictions;
- current punch material and coating;
- the actual failure seen in production.
Stainless applications often create high contact pressure, Tarcie ślizgowe, and heat at the punch surface. Under unfavorable conditions, workpiece material can transfer onto the punch. This adhesive wear process is commonly described as galling or material pickup.
Recenzowana recenzja naukowa Zgniatki w formowaniu metalowym explains that friction, Stan powierzchni, Ciśnienie, Temperatura, and wear development interact during the process. Once pickup begins, the roughened punch surface can attract more material, increase stripping force, damage the sheet surface, and accelerate further wear.
Stainless sheet may also work-harden near the cutting zone. Thicker or stronger material raises the load on the cutting edge. These conditions make it risky to choose a punch only by nominal hardness.
Wybierz podłoże dziurkowe przed wyborem powłoki
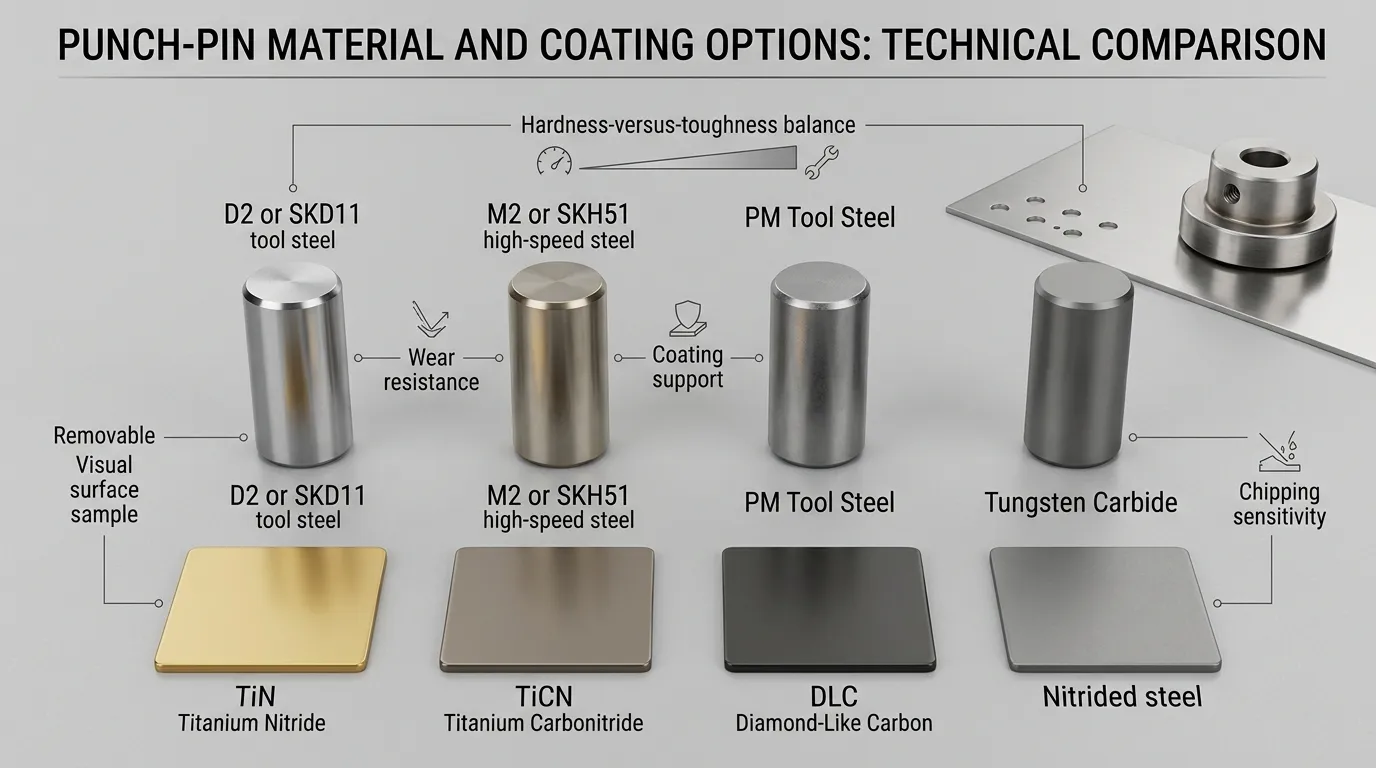
The coating is supported by the material underneath it. A hard coating on an unsuitable, poorly heat-treated, or damaged substrate can still crack, delaminate, chip, or fail with the cutting edge.
The main punch-material options should be compared using several properties:
| Podłoże dziurkowe | Główne zalety | Główne ograniczenia | Typowy powód, by to rozważyć |
|---|---|---|---|
| Stal narzędziowa typu D2 lub SKD11 | Odporność na zużycie, Wytrzymałość ściskająca, Stabilność wymiarowa | Can be less tolerant of impact, Odchylenie, or sharp stress concentrations than tougher grades | Stabilna geometria i umiarkowana produkcja oparta na zużyciu |
| M2, SKH51, or SKH9 HSS | Better balance of wear resistance, Wytrzymałość, oraz odporność na ciepło | Higher cost than conventional tool steel; still dependent on correct heat treatment | Stainless, thicker sheet, coated punches, or higher production demands |
| Stal narzędziowa PM | Silna równowaga zużycia i wytrzymałości oraz bardziej jednolita mikrostruktura | Wysoki koszt materiału oraz wymagania dotyczące konkretnego typu obróbki | Gdy konwencjonalna stal zużywa się zbyt szybko, a węglik jest zbyt kruchy. |
| Odporność na uderzenia stal narzędziowa | Wysoka wytrzymałość i odporność na pęknięcia związane z uderzeniami | Niższa odporność na zużycie niż w przypadku silnie stopowanych klas zużycia | Odpryski lub uderzenia są ważniejsze niż stopniowe zużycie |
| Węglik wolframu | Very high hardness, Wytrzymałość ściskająca, oraz odporność na zużycie | Brittle under misalignment, szok, Odchylenie, or poor edge support | Stabilna produkcja o wysokim zużyciu dzięki sztywnym oprawom |
| Stal narzędziowa ze stali nierdzewnej, taka jak SUS420 lub SUS440 | Odporność na korozję i polerowanie | To nie jest automatycznie najlepsze podłoże do przebijania arkuszy nierdzewnej | Środowiska korozyjne lub zastosowania, gdzie sam wykrawacz wymaga odporności na korozję |
D2 or SKD11 for Stable, Wear-Led Applications
D2-class cold-work tool steel is widely used where wear resistance and compressive strength are important. Material documentation for BÖHLER K110, a D2-class steel, lists stamping and blanking among its applications and emphasizes wear resistance and dimensional stability.
D2 or SKD11 may be a reasonable starting point when:
- the punch has a robust cross-section;
- alignment and clearance are controlled;
- production volume is moderate;
- gradual wear is the main concern;
- sudden chipping or bending is not occurring.
It becomes a weaker choice when the punch is very slender, has sharp corners, experiences side loading, or breaks before the cutting edge wears out. W takich przypadkach, additional hardness may make the problem worse rather than better.
M2, SKH51, or SKH9 When Toughness and Heat Resistance Matter More
High-speed steel is commonly evaluated when the punch needs a stronger balance of wear resistance, Wytrzymałość, and resistance to heat generated during repeated cycling.
Wskazówki techniczne z CONIC o materiałach narzędziowych associates M2-type material with stainless steel, thicker sheet, coating use, and larger production quantities. That does not make M2 a universal answer, but it explains why HSS often appears in stainless stamping recommendations.
SunshinePro's Dziurkarz do stali o dużej prędkości page lists SKH51 and SKH9 among its material options, along with vacuum heat treatment, precyzyjne szlifowanie, EDM, and optional TiN or TiCN coatings. These are company-specific product options, not fixed specifications for every application.
HSS is worth evaluating when:
- D2 wears or chips too quickly;
- surface heat is significant;
- the punch will receive a PVD coating;
- production volume justifies a higher-cost substrate;
- the geometry needs more fracture resistance than conventional wear steel provides.
Stal narzędziowa PM dla lepszego równowagi między zużyciem a wytrzymałością
Powder-metallurgy tool steels are useful when both wear and fracture resistance matter. Their more uniform microstructure can provide a better combination of properties than many conventionally produced tool steels.
Na przykład, the manufacturer describes BÖHLER K490 MICROCLEAN as a PM cold-work steel combining wear resistance, Wytrzymałość ściskająca, Wytrzymałość, and dimensional stability for applications that include stamping and blanking.
PM steel may be justified when:
- conventional D2-type steel wears too quickly;
- HSS does not provide the required service interval;
- carbide chips under the existing geometry or loading;
- downtime costs more than the material upgrade;
- repeated regrinding and stable dimensional behavior are important.
The recommendation must still be grade-specific. “PM steel” is a manufacturing category, not one standardized set of properties.
Carbide for Stable High-Wear Conditions, Not Every High-Volume Job
Tungsten carbide offers high hardness, Wytrzymałość ściskająca, and resistance to abrasive wear. It can be effective in stable, high-volume applications where the punch receives rigid support and loading remains predictable.
Its main limitation is brittleness. Carbide is less forgiving of:
- Niedopasowanie;
- Odbicie ciosu;
- impact or interrupted loading;
- weak corner geometry;
- niewystarczające wsparcie;
- slug interference;
- Boczny ładunek;
- Nieprawidłowe prześwitanie.
A carbide punch that chips after a few cycles is not improved by selecting an even harder carbide grade without correcting the mechanical cause.
SunshinePro's Wykrawające węglik page lists tungsten carbide, precyzyjne szlifowanie, EDM, customized dimensions, and TiN, TiCN, or DLC coating options. Suitability still requires a review of the punch geometry, Element obrabiany, Warunki prasowe, oraz historia awarii.
Gdy wybicie do stali nierdzewnej jest faktycznie wymagane
A punch used on stainless steel does not automatically need a stainless substrate.
Corrosion-resistant grades such as SUS420 or SUS440 may be selected when the tool itself is exposed to moisture, corrosive substances, frequent cleaning, or an environment where rust resistance matters. SunshinePro lists these grades on its separate stainless punch-pin product page.
That is a different engineering requirement from selecting a wear-resistant punch for stainless sheet. In many stamping applications, HSS, PM steel, conventional tool steel, or carbide may provide a more useful balance of wear, Wytrzymałość, and edge stability.
Dopasuj powłokę lub obróbkę powierzchni do trybu awarii
Coating choice should begin with the observed surface failure.
- Zużycie lub uszkodzenie adhezji: prioritize low friction, resistance to material transfer, Przygotowanie powierzchni, oraz smarowanie.
- Zużycie ścierne: prioritize surface hardness and resistance to gradual material loss.
- High heat: review thermal stability and compatibility with the substrate’s heat-treatment condition.
- Chipping or fracture: correct the substrate, Geometria, Przebieg trasy, or loading before focusing on the coating.
- Wysoka siła zdzierania: inspect pickup, Zakończenie, Smarowanie, and punch withdrawal conditions.
A coating name alone is not enough. Performance also depends on coating thickness, Przyczepność, Proces depozycji, edge preparation, substrate hardness, Temperatura pracy, oraz wykończenie powierzchni.
TiN and TiCN Are Common Options, Not Universal Answers
TiN is one of the most familiar hard coatings used on tooling. It can improve wear resistance in suitable systems, but it should not automatically be described as the preferred stainless-steel coating.
Na przykład, Wytyczne dotyczące powłoki Dayton Lamina assigns different treatments to adhesive wear, Zużycie ścierne, Ciepło, and specific work materials. Its recommendations also show that TiN is not universally preferred for stainless applications.
TiCN is commonly considered where higher wear resistance and improved sliding behavior are required. It may be evaluated for abrasive wear or material-pickup problems, but its performance still depends on substrate support, Przygotowanie powierzchni, coating quality, oraz warunki eksploatacji.
SunshinePro lists TiN and TiCN as available options on its HSS and stainless-steel punch-pin pages. The final selection should be based on the actual application rather than coating popularity.
AlTiN lub AlCrN dla warunków związanych z ciepłem
AlTiN and AlCrN coatings are often considered where elevated surface temperature and demanding wear conditions are central concerns.
Before selecting either coating, potwierdź:
- the substrate’s tempering resistance;
- coating-process temperature;
- required friction behavior;
- edge preparation;
- Przyczepność powłoki;
- whether heat or galling is the dominant failure.
A heat-resistant coating will not correct an unsupported edge or a punch that bends under load.
DLC i systemy wielowarstwowe Lubricious przeciwdziałanie zużyciu kleju
DLC and other low-friction multilayer systems may be considered where adhesive wear, irytujące, and high stripping force dominate.
Wskazówki techniczne od producentów narzędzi, takich jak Precyzja Mate connects low-friction coating selection with lubrication restrictions, punch dimensions, Grubość arkusza, and deflection. This is important because a lubricious surface can reduce friction, but it cannot stabilize a weak punch geometry.
DLC suitability depends on the substrate, Proces depozycji, service temperature, Przyczepność powłoki, and edge loading. SunshinePro lists DLC on its carbide-punch page, but that does not confirm availability or suitability for every punch material.
Nitridowanie, gdy zabieg dyfuzji pasuje do planu usług
Nitriding hardens the punch surface by diffusion rather than adding a separate deposited layer. It can be useful where surface hardness and geometry coverage are important.
Its selection should consider:
- substrate compatibility;
- Głębokość obudowy;
- Wymagane wykończenie powierzchni;
- Zmiana wymiarowa;
- Dodatek na ponowne szlifowanie;
- whether the treated layer will remain after sharpening.
Nitriding should not be described as a SunshinePro capability unless confirmed for the specific order. It remains a general technical option to discuss with the tooling and treatment supplier.
Zdiagnozuj awarię przed aktualizacją narzędzia
A more expensive material or coating is useful only when it addresses the actual failure.
| Zaobserwowany objaw | Prawdopodobny mechanizm | Sprawdź przed aktualizacją | Możliwy kierunek materiału | Możliwy kierunek powierzchni |
| Osad stali nierdzewnej na dziurku | Zużycie przez zwierzanie lub klej | Zakończenie, Smarowanie, Ciepło, Dostęp, stripping action | Zachowaj twarde podłoże, jeśli nie odkształca się ani nie odpryskuje | Low-friction PVD, DLC-type system, nitridowanie, or improved polishing depending on conditions |
| Stopniowe zaokrąglanie krawędzi | Zużycie ścierne | Workpiece condition, Dostęp, punch hardness, Produkcja | HSS, PM steel, or carbide if the process is stable | TiCN lub inna powłoka skupiona na zużyciu |
| Małe odpryski na krawędzi cięcia | Miejscowe pęknięcie lub niewystarczająca wytrzymałość | Geometria krawędzi, Przebieg trasy, Rogi, Wsparcie dziurkowe, Obróbka cieplna | Tougher HSS, PM steel, or shock-resistant steel | Nie traktuj powłoki jako głównego rozwiązania |
| Nagłe pęknięcie dziurka | Mechanical overload, Odchylenie, Niedopasowanie, or brittle substrate | Wskazówki, Aparat retainerowy, Dostęp, slug interference, Długość dziurka | Podłoże oparte na wytrzymałości po naprawieniu przyczyny mechanicznej | Powłoka jest wtórna |
| Odkształcenie krawędzi lub przewinięcie | Inadequate hardness, Wytrzymałość ściskająca, lub wsparcie | Obróbka cieplna, punch load, Grubość, Geometria | Higher-strength tool steel, HSS, PM steel, or carbide where stable | Powłoka ścierająca się dopiero po korekcji podłoża |
| Duża siła odwrotu | Przetwornik, poor stripping, Nierówne wykończenie, or inadequate lubrication | Stripper condition, punch surface, Smar, Boczny ładunek | Zachowanie wystarczającej wytrzymałości na obciążenie wyciągowe | Obróbka o niskim tarciu tam, gdzie jest kompatybilna |
Ogólna diagnoza złamań należy do osobnego przewodnika Pęknięcie dziurkownika w matrycach tłoczących. The critical point here is that chipping and breakage often indicate a bulk-material or mechanical problem, not a missing coating.
Sprawdź geometrię i warunki matrycy przed zrzuceniem winy na materiał
The punch operates as part of a complete die system. Before changing the substrate or coating, inspect the conditions that control how the load reaches the cutting edge.
- Confirm punch alignment. Misalignment creates uneven edge loading and can chip even a premium punch.
- Review punch-and-die clearance. Clearance should match the workpiece material and thickness. An unsuitable value can increase force, Formowanie żarna, zużycie, and fracture risk.
- Inspect the stripper and guide system. Poor guidance or abnormal stripping can bend the punch during withdrawal.
- Check the retainer and mounting condition. Movement at the head or shank changes how the punch is loaded.
- Inspect for slug interference. A trapped or pulled slug can create sudden overload.
- Review the punch surface. Grinding marks, Uszkodzenia, or pickup can accelerate galling.
- Confirm lubrication. Restricted lubrication changes the friction and coating requirements.
- Account for coating thickness. Final dimensions and tolerances should reflect the complete coated condition.
The Przewodnik po komponentach matrycy provides broader information about punches, Piny, tulejki, Komponenty przewodnika, and wear parts.
Małe i cienkie ciosy wymagają najpierw oceny wytrzymałości
A small-diameter or high-aspect-ratio punch can deflect before the cutting edge reaches its nominal material limit.
Risk rises when the punch has:
- Nadmierna długość bez podparcia;
- ostre narożniki;
- wąskie odcinki;
- Boczny ładunek;
- interrupted contact;
- Słabe wskazówki;
- heavy stripping force.
In this situation, selecting carbide or maximizing hardness can increase chipping risk. A tougher HSS or PM steel, krótsza długość bez podpory, stronger guidance, and improved corner design may provide a better result than a harder coating.
Wykorzystaj warunki aplikacji do wybrania systemu materiał–powłoki
The following matrix provides a starting direction, not a final engineering specification.
| Warunek aplikacji | Ocena kierunku podłoża | Kierunek powierzchniowy do oceny | Najpierw zweryfikowaj |
| Moderate volume, robust geometry, controlled process | D2/SKD11 lub HSS | Polished uncoated surface, TiN, TiCN, or nitriding depending on wear | Grade, Grubość, Dostęp, Smarowanie |
| Zużycie ścierne o dużej objętości | HSS, PM steel, lub węglik | Leczenie PVD skoncentrowane na zużyciu | Przebieg trasy, edge support, regrinding plan |
| Uszkodzenie widocznego materiału do przechwytu | Wytrzymała stal HSS lub PM, jeśli podłoże pozostaje stabilne | Low-friction PVD, DLC-type system, multilayer coating, or nitriding | Zakończenie, Smar, Ciepło, stripper action |
| Mały lub smukły punch z odpryskami | Tough HSS, PM steel, or shock-resistant steel | Powłoka dopiero po opanowaniu przyczyny złamania | Długość bez podparcia, Wskazówki, Rogi, Przebieg trasy |
| Gruba lub wysokoobciążeniowa blacha nierdzewna | HSS or PM steel; carbide only in a rigid, stable setup | Ciepło- and wear-appropriate coating | Punch load, Dostęp, Wsparcie, Warunki prasy |
| Środowisko narzędziowe o korozji | Odporna na korozję stal narzędziowa ze stali nierdzewnej tam, gdzie pozwala na to obciążenie | Zabieg zgodny z wybranym podłożem ze stali nierdzewnej | To, czy odporność na korozję czy wytrzymałość uderzeń jest głównym priorytetem |
Do not use this matrix to skip testing or drawing review. Two applications using the same stainless grade may need different punches because the thickness, hole diameter, Długość dziurka, Smarowanie, Szybkość prasy, and service expectations are different.
Porównaj opcje narzędzi według dostępności serwisowej i kosztu za trafienie
Initial purchase price is a weak basis for comparing punch options.
A more useful evaluation includes:
- hits between sharpening or replacement;
- unplanned downtime;
- tool-change frequency;
- regrinding cost;
- recoating feasibility;
- dimensional loss after sharpening;
- scrap and surface-damage risk;
- inspection time;
- Czas realizacji wymiany;
- probability of sudden fracture.
A PM steel or carbide punch may cost more at the start but reduce cost per hit in a stable application. The same upgrade can become expensive if the punch continues to break because of misalignment or poor guidance.
Regrinding also changes the tool. It can reduce punch length, remove the treated surface near the cutting edge, alter corner geometry, and affect shut height or penetration. Recoating is possible only when enough usable material remains and the surface can be restored to the condition required by the coating supplier.
The service plan should therefore be considered before the original material and coating are selected.
Informacje do uwzględnienia w indywidualnym RFQ do wykonywania pinów
A supplier cannot make a defensible recommendation from the phrase “punch for stainless steel” alone.
Include the following information in the request:
- stainless grade and family;
- Grubość arkusza;
- temper, Twardość, or tensile condition;
- part and hole drawing;
- punch diameter, Długość, głowa, Shank, and corner geometry;
- required dimensional tolerances;
- die clearance where known;
- press type and stroke rate;
- Przewidywana produkcja;
- target service interval;
- lubricant or dry-running restriction;
- current punch material and hardness;
- current coating or treatment;
- photographs or samples of wear, pickup, odpryskiwanie, or breakage;
- regrinding and recoating expectations;
- Materiały wymagane, Twardość, Wymiar, lub dokumentacja powłok.
SunshinePro states that it supplies standard components and non-standard customized parts processed from customer drawings. Its relevant punch pages list combinations of CNC machining, precyzyjne szlifowanie, EDM, Obróbka próżniowa, custom dimensions, HSS, Węglik, stainless tool steel, and selected coating options.
These website-confirmed capabilities should still be reviewed against the actual drawing and application. A tolerance or material listed on one product page should not be assumed to apply to every punch geometry.
Zasada ostatecznego wyboru
Use this order when selecting punch pins for stainless steel stamping:
- Identify the stainless grade, Stan, Grubość, and feature geometry.
- Determine whether the current failure is galling, Zużycie ścierne, odpryskiwanie, Uszkodzenie, lub deformacji.
- Correct alignment, Dostęp, Wskazówki, Zakończenie, Zdejmowanie, and lubrication problems.
- Select the substrate for bulk toughness, Wytrzymałość ściskająca, and edge stability.
- Select the coating or treatment for the dominant surface failure.
- Compare serviceability, Czas wolny, and cost per hit.
- Confirm the final system through drawing review and application-specific validation.
For a custom review, Prześlij rysunek, stainless specification, Warunki produkcyjne, and current failure details through SunshinePro’s Strona kontaktowa. That information gives the supplier a practical basis for evaluating the punch material, Obróbka cieplna, Zakończenie, Powłoka, oraz wymagania inspekcyjne.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
