



D2 vs M2 stal do sworzni dziurkaczowych: Zużycie, Wytrzymałość, oraz Speed
For punch pins, D2 and M2 solve different combinations of wear, Wpływ, and thermal stress. D2 is often a practical choice when gradual abrasive wear is the main concern and the die operates under controlled cold-work conditions. M2 may be the stronger candidate when the punch faces repeated edge chipping, difficult stock, long production runs, slender geometry, or sustained heat at the cutting edge.
Neither material is automatically better. Press speed alone does not determine the answer, and a harder punch is not always a more durable punch. Clearance, Obróbka cieplna, Geometria, Przebieg trasy, Smarowanie, and the actual failure pattern can matter as much as the steel grade.
Material selection is also only one part of a complete die system. The broader relationship between punches, to, Dostęp, and tooling requirements is covered in SunshinePro’s Przewodnik po formach wybicia (wnioskowane).
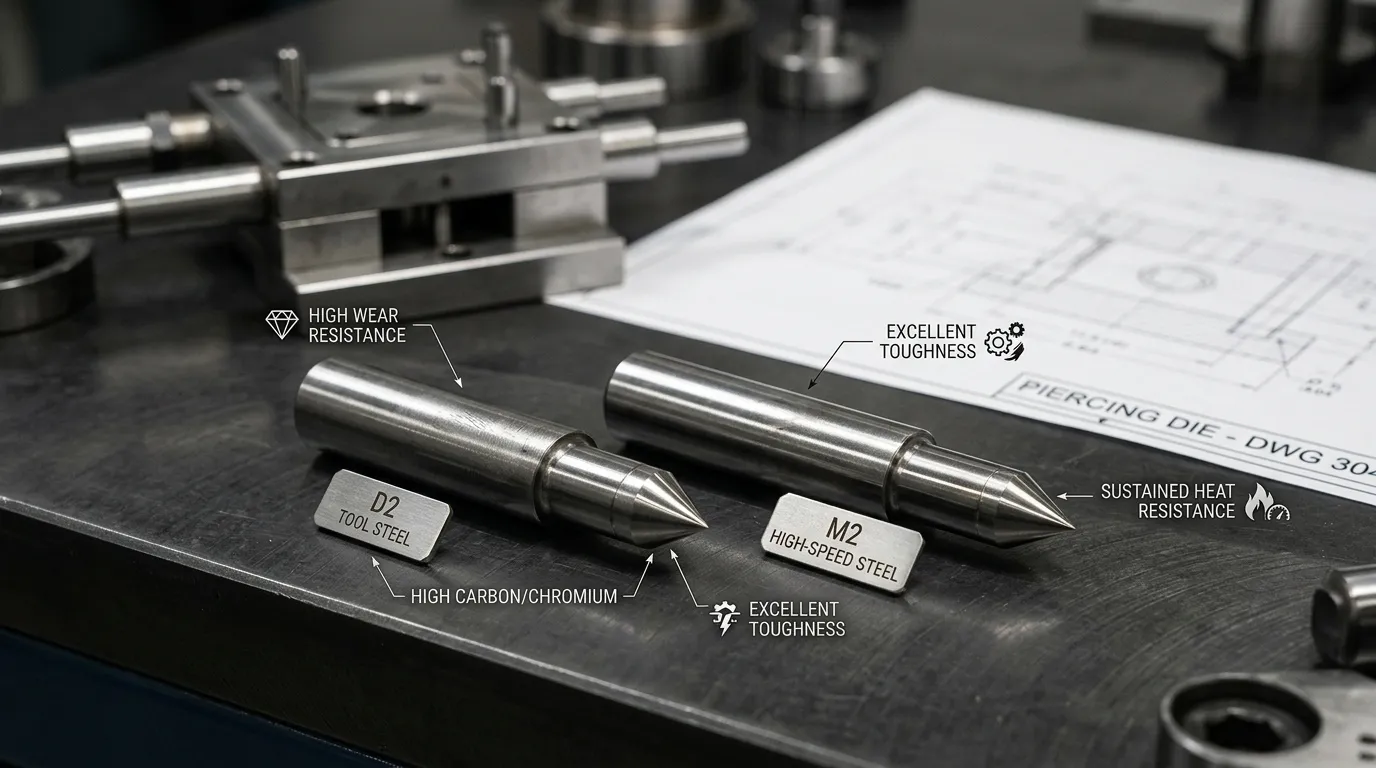
Porównanie sworzni dziurkowych D2 vs M2 na pierwszy rzut oka
| Czynnik porównawczy | Stal narzędziowa D2 | Stal szybkoobrotowa M2 |
|---|---|---|
| Rodzina stalowa | Stal narzędziowa do obróbki na zimno | Stal szybkościąca |
| Typical selection strength | Silna odporność na zużycie w kontrolowanych warunkach pracy na zimno | Balanced wear resistance, Stabilność krawędzi, Wytrzymałość, and hot hardness |
| Główne ograniczenie | Can become vulnerable to chipping or fatigue when the hardness, Geometria, or loading is too aggressive | Wyższe koszty materiału i obróbki mogą nie być uzasadnione w zastosowaniach umiarkowanych |
| Zużycie ścierne | Często jest silnym kandydatem tam, gdzie dominuje stopniowe ściernie | Also wear resistant, especially where wear occurs with heat or repeated impact |
| Wytrzymałość i odpryski | Zależność od aplikacji; geometry and heat treatment must be controlled | Często rozważane są miejsca, gdy D2 doświadcza powtarzającego się odprysku krawędzi w warunkach stabilnych |
| Ogrzewanie utrzymywane | Mniej odpowiedni do zastosowań, gdzie krawędź tnąca pozostaje gorąca przez dłuższy czas | Lepiej znany z utrzymywania twardości w podwyższonych temperaturach serwisowych |
| Warunki najlepszego dopasowania | Stable alignment, suitable clearance, controlled impact, moderate thermal demand | Long runs, difficult stock, higher thermal demand, Cienkie ciosy, or expensive downtime |
| Kierunek kosztów | Powszechnie uważane za bardziej ekonomiczny punkt wyjścia | Zazwyczaj oceniane, gdy poprawa niezawodności może zrekompensować dodatkowe koszty |
| Wymagana weryfikacja | Dokładny nachylenie, Obróbka cieplna, Twardość, Geometria, oraz warunki produkcji | Dokładny nachylenie, Obróbka cieplna, Warunki odpuszczania, Twardość, oraz warunki produkcji |
These are selection tendencies, not guaranteed performance rankings. A poorly supported M2 punch can fail before a correctly designed D2 punch, while an over-hardened or misaligned D2 punch can chip before its wear resistance becomes useful.
Dlaczego D2 i M2 zachowują się inaczej podczas ciosów
D2 is a high-carbon, high-chromium cold-work tool steel. It is commonly associated with wear resistance, compressive-load capability, and dimensional stability in tools operating without sustained high-temperature exposure. The BÖHLER K110 datasheet, which covers a D2-family grade, lists punching and stamping tools among its applications.
M2 belongs to the molybdenum high-speed-steel family. Its alloy system is designed to retain hardness and cutting performance under greater thermal demand. The BÖHLER S600 karta katalogowa, covering an M2-family grade, emphasizes wear resistance, Wytrzymałość, Stabilność krawędzi, Wytrzymałość ściskająca, and red hardness.
The difference cannot be reduced to a single Rockwell hardness value. Two punch pins at a similar HRC may still behave differently because of:
- Skład stopów i rozkład węglika
- Austenitizacja, Hartowanie, and tempering conditions
- Zachowana mikrostruktura
- Szlifowanie i stan powierzchni EDM
- Geometria dziurkownika i podparcie
- Temperatura podczas produkcji
- Rodzaj zużycia lub złamania, które występuje
The agreed material standard therefore matters. ASTM A681 covers alloy tool steels such as D2, podczas gdy ASTM A600 covers high-speed tool steels such as M2.
Nazwy klas, których kupujący nie powinni traktować jako automatycznych odpowiedników
Worldwide sourcing often involves several designation systems. D2 may be discussed alongside SKD11 or 1.2379, while M2 may be cross-referenced with SKH51, SKH9, or 1.3343.
These names should not be accepted as interchangeable without checking the applicable standard, chemia, production route, and final heat-treated condition. The drawing or purchase specification should identify the agreed grade rather than relying on a general trade name.
DC53 also should not be described as another name for standard D2. It is a separate modified cold-work steel with its own processing and performance characteristics.
Odporność na zużycie: Identify the Wear Mechanism Before Choosing
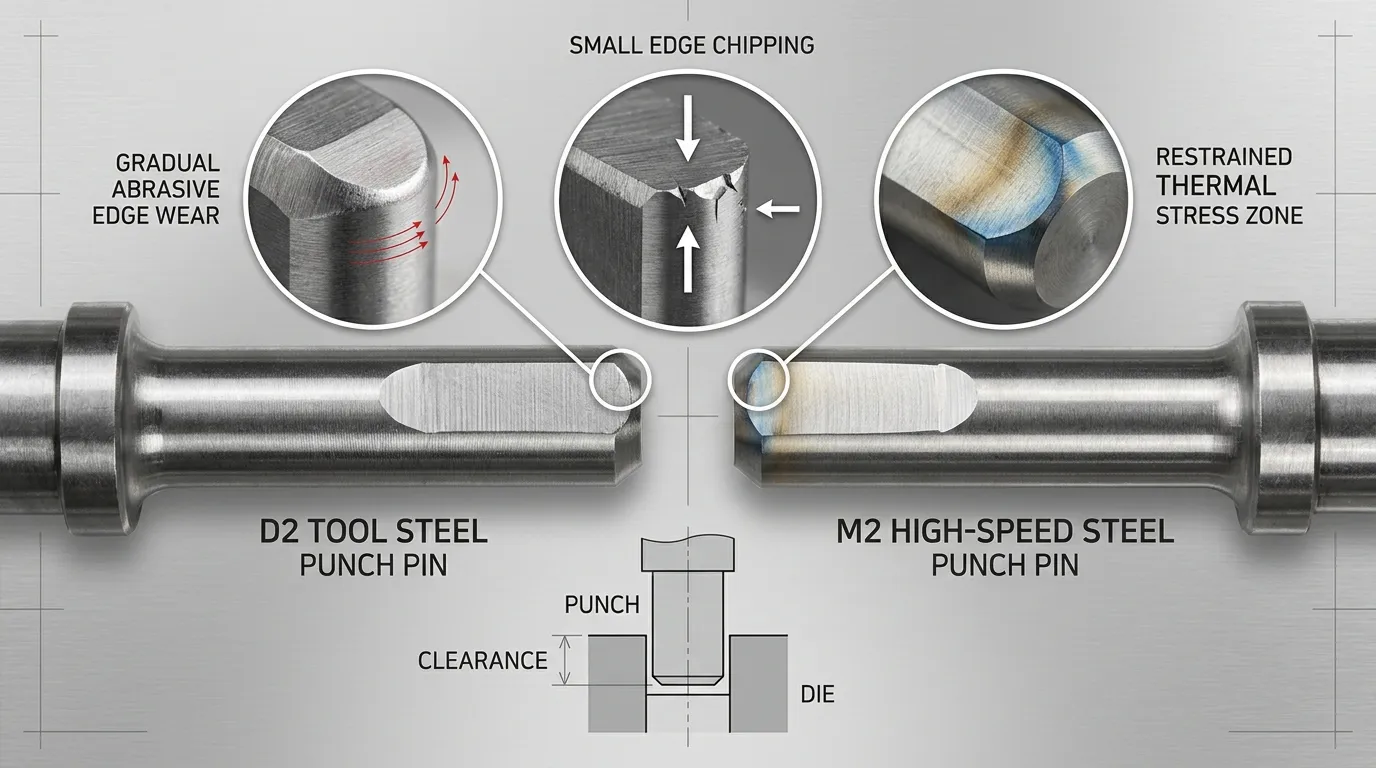
Asking which steel has “better wear resistance” is incomplete until the wear mechanism is known.
Zużycie ścierne gradually removes material from the punch edge or flank. It may be driven by hard particles, Skala, an abrasive workpiece, or repeated sliding contact. D2 is often considered when this predictable, gradual wear is the primary problem and shock loading remains controlled.
Zużycie kleju i uszkodzenia involve material transfer, pickup, or local seizure between the punch and workpiece. These problems are influenced heavily by workpiece material, Wykończenie powierzchni, Smarowanie, Dostęp, oraz powłoka. Changing from D2 to M2 may not correct galling if friction and material adhesion remain the real causes.
Zużycie połączone z odpryskami lub ciepłem creates a different selection problem. M2 may provide a more useful performance balance where the edge must resist abrasion while also tolerating repeated stress and sustained temperature.
Before changing steel, inspect how the existing punch is deteriorating:
| Obserwowany stan | Prawdopodobna kwestia do zbadania | Znaczenie materialne |
| Smooth, gradual edge recession | Zużycie ścierne | D2 may remain suitable; compare maintenance interval and total cost |
| Zbieranie materiału lub surowe osady | Galling, Zakończenie, Smarowanie, Powłoka | Popraw warunki powierzchniowe przed obwinieniem stali masowej |
| Małe kawałki odłamujące się od krawędzi | Odpryskiwanie, Nadmierna twardość, Geometria, Dostęp, Boczny ładunek | M2 można rozważyć po kontrolowaniu przyczyn układu |
| Szybkie zużycie podczas długich, nieprzerwanych kursów | Ścieranie mieszane i ciepło | Zdolność M2 do twardości na gorąco może stać się bardziej istotna |
SunshinePro’s die punch pin page lists precision grinding and TiN and TiCN coating options. These processes can support surface condition and wear control, but a coating cannot compensate for unsuitable steel, Słabe ustawienie, Nieprawidłowe prześwitanie, or weak punch support.
Wytrzymałość, Odpryskiwanie, and Punch Geometry
Punch toughness is not determined by the steel name alone. The final hardness, Obróbka cieplna, edge shape, Długość bez podparcia, and loading direction all affect whether the punch bends, Chipy, or develops fatigue cracks.
A large, well-supported round punch and a long, narrow punch do not place the same demands on the material. Small-diameter punches, sharp internal features, narrow points, and long unsupported sections create greater stress concentration and bending risk.
Repeated chipping can result from:
- Nadmierna twardość dla geometrii
- Nieprawidłowy prześwit od dziurkania do matrycy
- Słabe prowadzenie lub ustawienie
- Boczny ładunek
- Niewystarczające wsparcie głowy lub ciała
- Obrażenia od grindowania
- Warstwa niekontrolowanego EDM recast
- Wady obróbki cieplnej
- Przeciążenie lokalne spowodowane zmianami w fabryce
A published failure analysis of an AISI D2 punch found that punch damage could involve fatigue, carbide cracking, excessive loading, heat-treatment issues, backup-plate wear, Dostęp, and guiding conditions. The study reinforces a basic rule: changing the material without correcting the mechanical cause may only move the failure to another location. Zobacz badanie na zmęczenie i zużycie w ciosu AISI D2.
M2 may deserve evaluation when a D2 punch repeatedly chips despite correct alignment, suitable clearance, stable heat treatment, and adequate support. It should not be treated as a substitute for investigating the die system. A more complete diagnosis of side loading, Dostęp, Przewodnictwo, and fracture causes belongs in the guide to Pęknięcie dziurkownika w matrycach tłoczących.
Gdy szybkość nacisku sprawia, że twardość M2 na gorąco ma znaczenie
The term “high-speed steel” often leads to an oversimplified rule: fast press equals M2. Actual punch conditions are more complicated.
Strokes per minute affect the number of loading events, but they do not directly state the cutting-edge temperature. Thermal demand also depends on:
- Ciągły czas trwania
- Wytrzymałość i grubość obrabianego elementu
- Rozmiar otworu i geometria dziurkacza
- Prześwit od dziurka do wydruku
- Tarcie i żarlienie
- Smarowanie
- Rozpraszanie ciepła między suwami
- Czas trwania i częstotliwość zatrzymania produkcji
A fast press running short batches of thin, manageable stock may produce less sustained edge heat than a slower press running thick, high-strength material continuously.
M2’s hot hardness becomes more valuable when the cutting edge remains hot enough for ordinary cold-work performance to deteriorate. That condition may appear during long progressive-die runs, difficult stock punching, wysokie tarcie, or inadequate cooling between cycles.
D2 can still be suitable at a high numerical press speed when thermal load, Wpływ, and chipping risk remain controlled. M2 should therefore be selected because of the complete duty cycle, not because the press specification contains a high strokes-per-minute number.
D2 or M2? Choose by Failure Mode and Application
The following table provides a starting direction. It is not a substitute for examining the die, Element obrabiany, Obróbka cieplna, and failed punch.
| Warunek aplikacji | Prawdopodobny kandydat na start | Powód | Sprawdź przed podjęciem decyzji |
| Stabilność, gradual abrasive wear | D2 | Silna odporność na zimno może być wystarczająca | Twardość, Interwał wyostrzenia, stock abrasiveness |
| Krawędź D2 wielokrotnie się wykręca | M2 może być oceniany | Szersza wytrzymałość i równowaga między stabilnością krawędzi a stabilnością może pomóc | Clearance, Przebieg trasy, Geometria, Obróbka cieplna |
| Długa nieprzerwana produkcja z utrzymującym się nagrzewaniem krawędzi | M2 | Twardość na gorąco staje się bardziej istotna | Actual temperature drivers, tarcie, Smarowanie |
| Dziurkacz o małej średnicy lub smukłości | M2 może być oceniany | Geometria może wymagać większej odporności na odpryski i zmęczenie | Długość bez podparcia, Przewodnictwo, Podpora głowy |
| Umiarkowane wybijanie miękkie lub węglowe | D2 może być wystarczające | Zapotrzebowanie na ciepło i uderzenia może nie uzasadniać M2 | Stock thickness, Dostęp, desired maintenance interval |
| Materiał ze stali nierdzewnej lub podatny na żalenia | Zależność od aplikacji | Tarcie, Przyczepność, and heat may dominate | Smarowanie, Wykończenie powierzchni, Powłoka, Dostęp |
| Gruba lub o wyższej wytrzymałości blacha | M2 może mieć przewagę | Wyższe obciążenia mogą zwiększać naprężenia krawędzi i ciepło | Średnica dziurka, press force, Wsparcie, hole geometry |
| Przestoj jest znacznie droższy niż koszt narzędzi | M2 może być ekonomicznie uzasadniony | Dodatkowy koszt początkowy może być akceptowalny, jeśli niezawodność się poprawi | Rekordy produkcyjne i wyniki badań kontrolowanych |
Typowe warunki, w których D2 może być wystarczające
D2 remains a reasonable candidate when the punch experiences predictable wear under stable cold-working conditions. Suitable clearance, strong guidance, adequate support, and controlled hardness allow its wear resistance to be used without excessive chipping.
It can be a practical choice for moderate production duties where current sharpening intervals are acceptable and the application does not create sustained heat or severe impact.
Warunki, w których M2 może uzasadniać wyższy koszt
M2 becomes more attractive when a punch must maintain its edge under combined wear, repeated stress, and thermal demand. Examples include long production runs, difficult or higher-strength stock, slender punch geometry, and applications where recurring D2 chipping continues after system problems have been corrected.
The economic case is strongest when unplanned breakage or press downtime costs much more than the difference in punch material and processing.
Steel Grade Alone Will Not Fix Clearance, Przebieg trasy, or Heat-Treatment Problems
Before replacing D2 with M2, confirm that the current punch is being tested fairly. Co najmniej, Recenzja:
- Prześwit od dziurka do wydruku
- Koncentryczność i wyrównanie uderzenia
- Stan słupka prowadzącego i tulejki
- Wsparcie dziurkowana i długość bez podparcia
- Różnice grubości i twardości obrabianego elementu
- Spójność smarowania
- Oparzenia szlifujące lub obrażenia krawędzi
- Stan powierzchni EDM
- Ostateczna twardość i warunki odpuszczania
- Stan powłoki
- Wzór zużycia na otworze dziurkacza i matrycy
Incorrect clearance can increase cutting load, Formowanie żarna, edge stress, oraz odpryskiwania. Misalignment can place bending loads on a punch designed mainly for compression. Grinding or EDM damage can also provide a starting point for fatigue cracks.
A punch works as part of a larger assembly. The relationship between the punch, Aparat retainerowy, Przewodniki, tulejki, die insert, and support components is covered more broadly in the Przewodnik po komponentach matrycy.
Compare Cost by Downtime and Maintenance, Not Steel Price Alone
D2 may have a lower initial cost in many sourcing situations, but purchase price does not show the complete economic result. M2 may cost more to purchase, Maszyna, heat-treat, or grind, yet still be worthwhile if it reduces expensive production interruptions.
A useful comparison should include:
| Współczynnik kosztów | Pytanie do oceny |
| Początkowy koszt dziurkania | What is the delivered cost in the specified grade and condition? |
| Ostrzenie | How many hits occur between scheduled sharpening events? |
| Nieplanowane uszkodzenie | Does the punch wear predictably or fail without warning? |
| Przerwy | How much production is lost during replacement and die adjustment? |
| Złom | Does edge deterioration affect burrs, Wymiary, or part quality? |
| Inwentarz | How many spare punches are required to protect production? |
| Praca konserwacyjna | How much toolroom time is spent inspecting, ostrzenie, and replacing punches? |
M2 is not automatically the lower-cost choice. It becomes economically attractive only when its performance under the actual application reduces enough maintenance, failure, złom, or downtime to offset the added cost.
Co należy określić przed złożeniem wniosku o sworzeń D2 lub M2 do dziurkania
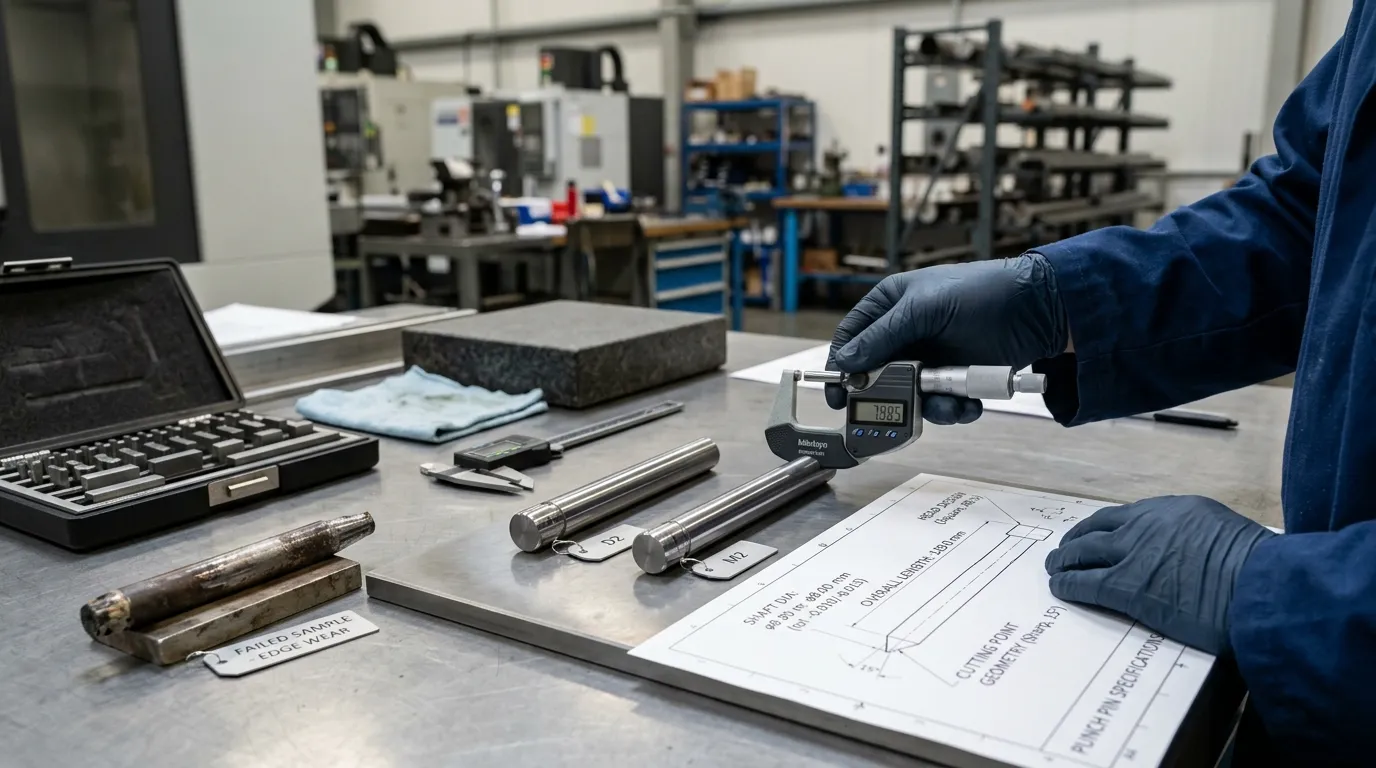
A supplier cannot make a reliable material recommendation from the punch diameter alone. The RFQ should describe both the component and its operating conditions.
Dostarczaj:
- Rysunek wymiarowy
- Średnica dziurka, Długość, and unsupported length
- Projekt głowicy i układ podparcia
- Point shape, corner radii, and special cutting features
- Materiał i naniesienie elementu obrabianego
- Grubość arkusza
- Wymiary i kształt otworów
- Prześwit od dziurka do wydruku
- Typ prasy i prędkość pracy
- Ciągły czas trwania
- Oczekiwana roczna liczba hitów
- Smar i metoda aplikacji
- Istniejący materiał dziurkowy i zmierzona twardość
- Current failure symptom: zużycie, irytujące, odpryskiwanie, bending, lub zmęczenie
- Fotografie lub próbki nieudane tam, gdzie są dostępne
- Wymagana powłoka
- Uzgodnione oznaczenie materiałowe i standard
- Wymagany certyfikat materiałowy
- Dokumentacja obróbki cieplnej
- Wymóg inspekcji twardości
- Kryteria akceptacji do testu produkcyjnego
SunshinePro states that non-standard components can be produced from customer drawings. To Strona produktu z wybicikiem lists custom diameter, Długość, Konstrukcja głowicy, Materiał, oraz opcje powłok, together with SKH51, SKH9, DC53, Stopnie ASP, oraz węglik. The page also mentions CNC machining, precyzyjne szlifowanie, EDM, oraz obróbkę cieplną próżniową.
That information does not confirm AISI D2 availability. Buyers requiring D2 should ask the supplier to confirm the exact material designation, applicable standard, Warunki obróbki cieplnej, and documentation before ordering.
A controlled trial remains the most reliable final check. Compare D2 and M2 using the same drawing, Dostęp, Prasa, workpiece batch, Smar, Status powłoki, oraz metodę inspekcji. Record the hit count and actual failure mechanism rather than judging only by whether the punch still appears usable.
Gdy ani konwencjonalne D2, ani M2 nie są właściwą odpowiedzią
If both materials fail after clearance, Wsparcie, Przebieg trasy, Smarowanie, Geometria, and heat treatment have been corrected, the application may require a different solution.
Possible next steps include reviewing:
- Stal szybkotnąca w metalurgii proszkowej
- Węglik
- Inny system powłok
- Zmieniona geometria dziurkacza
- Lepsze prowadzenie lub wsparcie
- Zmiany w przeświecie lub smarowaniu
SunshinePro lists ASP grades and carbide among its punch-pin material categories, but these alternatives should be evaluated against the same application data rather than treated as automatic upgrades.
For a material review or quotation, submit the punch drawing, Szczegóły elementów obrabianych, Warunki produkcyjne, and current failure evidence through the Strona kontaktowa SunshinePro. The strongest recommendation will come from matching the steel, Obróbka cieplna, Geometria, and die conditions to the failure mode the punch must actually survive.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
