



Nieprawidłowe ustawienie sworzni do pozycjonowania formy: Objawy i rozwiązywanie problemów
Mold positioning pin misalignment can cause binding during closure, Nierówny kontakt, parting-line mismatch, Błysk, abnormal wear, or inconsistent part dimensions. The pin itself may be damaged, Ale to tylko jedna z możliwych przyczyn. A worn bushing, loose mounting bore, contaminated parting surface, damaged interlock, Wzrost termiczny, poor mold installation, or machine-platen condition can create similar symptoms.
The correct approach is to identify when the problem occurs, inspect the entire mating system, measure the suspected geometry, and repair only the verified cause. For broader information about component fit, zużycie, Materiały, oraz smarowanie, see SunshinePro’s guide to Sworznie i tuleje formowe (wnioskowane).
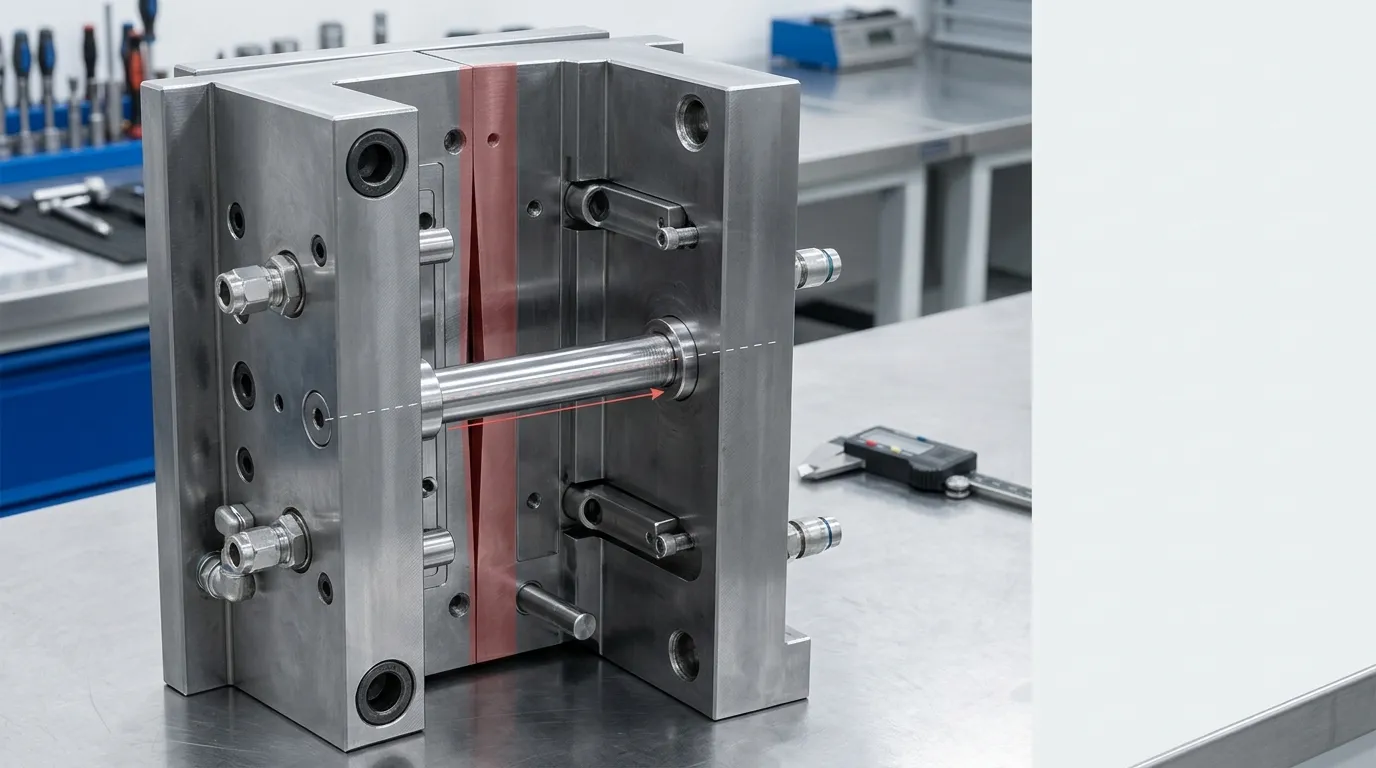
Najpierw sprawdź, co robi "pin" pozycjonujący w tej formie
“Positioning pin” is not used consistently across every mold design. Before troubleshooting, identify the component by function rather than relying only on its name.
| Składnik | Główna rola | Implikacje diagnostyczne |
|---|---|---|
| Locating or dowel pin | Ustala powtarzalną pozycję między komponentami lub płytami | Check its geometry, Montaż, Orientacja, and mating hole or bushing |
| Sworzeń prowadzący, leader pin, or guide pillar | Prowadzi połowy formy podczas zaangażowania | Sprawdź prostość, zużycie, bushing clearance, and side-loading marks |
| Prowadnica lub tulejka lokalizująca | Odbiera pin i steruje interfejsem łączącym | Check bore wear, ovality, Pozycja, Utrzymanie, and entry damage |
| Blokada boczna lub stożkowa blokada | Pomaga ustalić lub utrzymać ostateczną rejestrację pleśni | Check contact pattern, zużycie, Uszkodzenia, oraz zaangażowanie |
| Powierzchnia odcinająca lub precyzyjne dopasowanie | Przyczynia się do ostatecznego wyrównania i uszczelnienia | Check for impact marks, Niedopasowanie, local gaps, and edge damage |
A guide pin may control the initial closure path while another locating feature controls final core-to-cavity registration. Replacing the guide pin will not solve the problem if the final interlock, bushing, mounting bore, or mold plate is out of position.
Osobny przewodnik SunshinePro do Sworznie prowadzące formę covers broader guide-pin function, zużycie, and selection. Proszę, the focus is determining why an installed mold is no longer aligning correctly.
Objawy wskazujące na problem z rejestracją pleśni
The timing and location of a symptom often provide more useful evidence than the symptom alone.
| Objawy | Kiedy się pojawia | Możliwy podsystem | Pierwsza kontrola potwierdzająca |
| Wiązanie w tym samym miejscu podczas zamykania | Zamknięcie zimne lub bez obciążenia | Zgięty sworzeń, skewed bushing, damaged interlock, burr, or plate-position error | Zatrzymaj się w pierwszym punkcie kontaktu i sprawdź pod kątem jednostronnych śladów świadka |
| Scraping, drgania, or impact noise | Podczas zapinania sworzni lub blokady | Boczny ładunek, insufficient clearance, Zanieczyszczenie, or damaged entry geometry | Inspect the pin, bushing mouth, interlocks, and nearby surfaces |
| Nienormalne nagrzewanie w pobliżu systemu prowadzącego | Po wielokrotnych jazdach na rowerze | Tarcie, słabe smarowanie, tight fit, Boczny ładunek, or galling | Sprawdź punktację, Przebarwienia, Stan smaru, and uneven contact |
| Pleśń nie zamyka się dokładnie | Konfiguracja lub kontrolowane zamykanie | Mounting error, Przeszkoda, Zniekształcenie płyty, machine-side alignment, or damaged positioning components | Inspect mounting, Cechy lokalizujące, parting surfaces, and plate relationships |
| Etap rozdzielania lub niedopasowanie | W trakcie produkcji | Registration loss, Ruch płyty, interlock wear, or machine-side loading | Porównaj miejsce niezgodności z kontaktem i wzorcami zużycia |
| Zlokalizowana lampa błyskowa | Pod ciśnieniem wtrysku | Misregistration, damaged shutoff, insufficient clamping, Zanieczyszczenie, or process conditions | Sprawdź, czy forma ustawia się bez ciśnienia i sprawdź uszkodzony odcinek |
| Zmienność wymiarowa między cyklami | Po rozgrzewce lub pod obciążeniem | Changing clearance, Wzrost termiczny, Ruch płyty, or worn positioning features | Compare cold, warm, and production-condition measurements |
| Polerowanie jednostronnych sworzni lub tulejów | Postęp w czasie | Mispositioned bore, bent pin, plate error, or uneven machine loading | Zmierz wycięcie sworzni i sprawdź położenie otworu oraz prostopadłość |
DME’s technical guidance on mold interlocks identifies flash, dimensional problems, and component damage as possible consequences of improper mold alignment. It also notes that worn leader pins and bushings, thermal variation, mold weight, and equipment condition can affect registration. See DME’s Techniczne wskazówki dotyczące wyrównania formy.
Flash alone does not prove positioning pin failure. Flash can also result from damaged shutoffs, trapped material, insufficient clamping, excessive pressure, or other tooling and process conditions. Treat it as evidence that requires further inspection.
Objawy podczas zamykania pleśni
Closure-related symptoms usually point toward the engagement path.
Szukaj:
- Resistance that begins at the same position during each closing attempt.
- A pin entering the bushing off-center.
- Fresh contact marks on only one side of the pin.
- Scraping at the bushing entrance.
- Impact marks on interlocks or shutoffs.
- A visible gap on one side of the parting line.
- A pin, bushing, or retainer moving in its mounting feature.
A repeatable hard-contact point is more likely to involve geometry, Przeszkoda, or mounting position than a process-setting problem.
Objawy na formowanej części lub powierzchni rozdzielającej
Production evidence may include:
- A step across the parting line.
- Flash concentrated in one region.
- Uneven witness lines.
- Chipping or peening near a precision shutoff.
- Dimensional changes after the mold reaches operating temperature.
- Parts that shift in one direction under pressure but appear acceptable during an unloaded closure check.
These symptoms help locate the affected region, but measurements are still needed before deciding which component to repair.
Przestań cyklizować pleśń, gdy istnieje ryzyko uszkodzenia
Do not continue closing the mold to “see if it clears” when there is evidence of hard interference or displaced components.
Stop and establish a safe inspection condition when you find:
- A visibly bent or loose pin.
- A cracked, odcięte, or displaced bushing.
- Metal fragments or severe scoring.
- Fresh impact damage on a core, Ubytek, Insert, shutoff, or interlock.
- Sudden hard resistance during closure.
- A plate or component moving inside its mounting feature.
- An engagement path that cannot be confirmed safely.
Injection molding machines can expose technicians to crushing, stored hydraulic energy, electrical energy, hot surfaces, and moving components. Inspection and servicing should follow the machine manufacturer’s instructions, the facility’s hazardous-energy procedure, and applicable local regulations. USA. Occupational Safety and Health Administration provides general guidance on Zagrożenia związane z poziomymi maszynami do formowania wtryskowego oraz control of hazardous energy.
Rozwiązywanie problemów z nieprawidłowym ustawieniem w stałej kolejności
A consistent sequence reduces unnecessary disassembly and prevents one symptom from being mistaken for proof of pin failure.
- Review when the problem started.
Determine whether the change was sudden or progressive. Check whether it began after maintenance, Wymiana komponentów, mold transfer, machine setup, a cooling change, or warm-up. - Place the machine and mold in an approved safe inspection condition.
Isolate hazardous energy before entering the mold area or touching components that could move. - Clean exposed interfaces.
Remove trapped plastic, Chipy, burrs, contaminated lubricant, and other debris from the parting line, pin entries, tulejki, and interlocks. - Inspect the pin, bushing, Montaż, oraz utrzymanie.
Look for looseness, Punktacja, impact marks, nierówne polerowanie, Wyporność, or damaged fasteners. - Observe the engagement pattern.
Under an approved controlled procedure, identify which component contacts first and whether the contact is centered or one-sided. - Measure the suspected geometry.
Check pin and bushing dimensions, runout, Stan montażu, component position, and plate relationships. - Separate mold-side causes from machine-side and thermal causes.
Compare cold and warm behavior, unloaded and production-loaded behavior, and results across machines when practical. - Correct the verified cause.
Czyste, adjust, Naprawa, or replace only after the inspection evidence supports that action. - Validate the repair.
Confirm smooth engagement, stable registration, correct parting-line contact, and acceptable molded-part results.
Zapisz moment, gdy problem się zaczął
The failure history can quickly narrow the investigation.
A sudden problem after maintenance may indicate:
- A reversed or incorrect replacement component.
- A bushing or pin installed at the wrong depth.
- A burr created during assembly.
- A loose retainer or fastener.
- A plate assembled out of position.
Progressive deterioration more often suggests:
- Increasing pin or bushing wear.
- Lubrication breakdown.
- Mounting-bore damage.
- Plate movement.
- Repeated side loading.
- Thermal or machine conditions that gradually accelerate wear.
A problem that appears only after moving the mold to another machine should trigger checks of mold installation, locating-ring engagement, platen condition, and clamping alignment before replacing mold components.
Zacznij od czyszczenia i inspekcji nieniszczącej
Begin with checks that do not alter the mold:
- Clean pin surfaces and bushing entrances.
- Remove plastic residue from the parting line.
- Inspect for burrs around bores and interlocks.
- Check retainers and fasteners for movement.
- Mark and photograph contact patterns.
- Compare the left and right sides of the mold.
- Check whether the pin enters the bushing concentrically.
Cleaning may restore movement when debris is the only obstruction. It does not prove that the pin, bushing, or plate geometry remains within specification.
Sprawdź szpilkę, Tuleja, and Mounting Features as One System
A positioning pin does not work independently. Its performance depends on the mating bushing or hole, the mounting bore, the mold plate, and any final-positioning features.
Wskazówki dotyczące awarii strony kręgli.
Evidence that directly implicates the pin includes:
- Measurable bending or runout.
- One-sided scoring along the engagement length.
- Impact damage at the leading end.
- Mushrooming or chipped edges.
- A loose shank or failed retaining feature.
- Incorrect installed height.
- Geometry that does not match the drawing.
- Contact concentrated in one region rather than distributed as intended.
One-sided polishing can indicate a bent pin, but it can also result from a mispositioned bushing or mounting bore. Confirm the pin’s straightness before assigning the cause.
Tuleja- and Bore-Side Failure Clues
Inspect the mating side for:
- Uneven or oval bore wear.
- A loose bushing.
- Damage at the entry chamfer.
- Scoring concentrated on one side.
- A bushing installed out of position.
- Cracks or deformation around the mounting feature.
- A damaged press-fit bore.
- Burrs that prevent the bushing from seating correctly.
Replacing a worn pin while leaving an oval or loose bushing in place may restore movement temporarily without restoring repeatable registration. The mating pair and both mounting features should be evaluated together.
Zmierz geometrię przed wyborem naprawy
Visual inspection identifies where to investigate, but dimensional evidence should determine whether a component is acceptable.
Measure as applicable:
| Cechy | Dlaczego to ma znaczenie | Podstawa akceptacji |
| Średnica sworzni w kilku pozycjach | Reveals taper, localized wear, or material loss | Zatwierdzony rysunek formy lub specyfikacja komponentu |
| Tuleja była w kilku orientacjach | Identyfikuje nadmierne prześwicie lub zużycie owalne | Rysunek, supplier specification, or applicable standard |
| Prostość kręgli lub runout | Wykrywa zgięcie powodujące progresywny kontakt boczny | Procedura rysunku lub zatwierdzona inspekcja |
| Pozycja sworzni i tulejki | Określa, czy ich osie się wyrównują | Rysunek formowy i struktura data odniesienia |
| Prostopadłość do płyty | Identyfikuje pochyloną instalację lub błąd otworu | Rysunek lub specyfikacja inżynierska |
| Stan montażu cylindra | Określa, czy dany komponent jest odpowiednio wspierany i zachowany | Rysunek i zatwierdzone kryteria napraw |
| Relacja między płytą a płytą | Detects shift, Zniekształcenie, or movement between assemblies | Rysunki i plan inspekcji montażu formy |
Do not apply one universal pin-to-bushing clearance or wear limit to every mold. The correct value depends on the component design, Rozmiar, Funkcja, supplier series, Temperatura pracy, and required positioning accuracy.
For standardized components within their stated scope, ISO 8017 covers dimensions and tolerances for specified guide pillars and locating guide pillars. ISO 8018 covers specified headed guide and locating guide bushes. These standards do not replace the approved mold drawing, and they should not be applied to components outside their scope.
Record the measurement reference, Instrument, Przygotowanie, Poprawka rysunku, and actual results. A list of numbers without the measurement method may not be sufficient for repair or replacement decisions.
Oddzielne przyczyny po stronie formy od efektów maszynowych i temperaturowych
The same mold symptom can originate outside the pin-and-bushing pair.
Ask:
- Did the problem begin after installing the mold on a different machine?
- Does the mold align when cold but bind after warm-up?
- Does it close smoothly without pressure but shift during production?
- Is one mold half operating at a different temperature?
- Are the locating ring and mounting surfaces seated correctly?
- Are the platens, Zaciski, or tie system applying uneven load?
- Do interlocks show contact only after pressure is applied?
- Does the problem disappear when the mold is checked outside the original machine?
Niedopasowanie zimno kontra gorąco
A mold may close correctly at room temperature and begin binding after thermal stabilization. Unequal heating changes the dimensions of plates, bores, Piny, tulejki, and interlocks. The pin may appear to be the problem even though the underlying cause is differential thermal growth.
Compare:
- Cold engagement.
- Engagement during warm-up.
- Stable operating-temperature engagement.
- Temperatures on both mold halves.
- Cooling conditions near the affected region.
- Contact marks before and after warm-up.
Do not assume the pin changes independently of the surrounding plate. The entire alignment chain expands and moves together.
Nieobciążenie kontra niewyrównanie pod ciśnieniem
Smooth unloaded closure does not guarantee stable registration during production.
If misalignment appears only under injection or clamping load, Sprawdź:
- Side interlocks and taper locks.
- Plate support and fasteners.
- Shutoff contact.
- Mold mounting.
- Platen condition.
- Locating-ring engagement.
- Load-sensitive movement between plates.
Changing pressure, prędkość, or clamping settings may reduce the visible defect, but it does not correct a mechanical positioning error.
Dopasuj działanie naprawcze do zweryfikowanej przyczyny
| Zweryfikowana przyczyna | Odpowiednie działania | Additional check |
| Trapped plastic, Chipy, or removable debris | Oczyść dotknięte powierzchnie | Upewnij się, że nie pozostał żaden zadzior ani trwałe uszkodzenia |
| Zanieczyszczony lub brakujący zatwierdzony smar | Oczyść i przywrócić określony stan smarowania | Inspect for existing scoring, zużycie, or galling |
| Bent, worn, or impact-damaged pin | Zamień na komponent odpowiadający zatwierdzonemu rysunkowi | Sprawdź tulejkę i otwory montażowe |
| Zużyta lub owalna tuleja | Wymień lub napraw zgodnie z wzorem formy | Potwierdź stan sworzni i faktyczne warunki dopasowania |
| Luźny sworzeń lub tulejka | Popraw funkcję mocowania lub montażu poprzez zatwierdzoną naprawę | Sprawdź, czy otwor lub płyta nie są uszkodzone |
| Uszkodzona średnica montażowa | Napraw otwor lub uszkodzoną płytę przed zamontowaniem nowego komponentu | Przywrócenie pozycji i prostopadłości |
| Zużyty blok lub wyłącznik | Napraw lub wymień uszkodzoną funkcję końcowego pozycjonowania | Potwierdzaj, że komponenty przewodnika nie zostały załadowane z boku |
| Błąd instalacji lub nalokowania pierścienia | Prawidłowe montaż formy i centrowanie formy | Ponowne sprawdzenie zamknięcia i kontakt z linią rozdzielenia |
| Ładowanie po stronie maszyny lub wydawanie płyty | Postępuj zgodnie z procesem inspekcji i naprawy maszynowego | Potwierdź, że pleśń nie ucierpiała wtórnie |
| Zniekształcenia termiczne | Skoryguj zweryfikowaną nierównowagę temperaturową lub chłodzenie | Zweryfikowaj wyrównanie przy stabilnej temperaturze pracy |
Lubrication can reduce friction. It cannot straighten a bent pin, correct a misplaced bore, restore an oval bushing, or realign a distorted plate.
Do not install a new pin into a damaged bore simply because the replacement fits initially. If the mounting feature cannot hold the component at the required position and angle, the new part may fail quickly or reproduce the same alignment error.
Zweryfikowanie ustawienia przed powrotem formy do produkcji
After correction, validate the complete system rather than checking only whether the mold can close once.
Use the machine manufacturer’s approved procedure to confirm:
- Smooth and repeatable engagement.
- No abnormal impact, scraping, drgania, or resistance.
- No new scoring or concentrated witness marks.
- Correct parting-line and shutoff contact.
- Stable pin and bushing temperatures.
- No movement at retainers or mounting features.
- Consistent behavior after the mold reaches operating temperature.
- Stable registration under approved production conditions.
- Acceptable molded-part dimensions.
- No abnormal flash or parting-line step.
Recheck critical dimensions when a pin, bushing, Otwor, Tablica, or interlock has been repaired. Record what was changed, the measurements taken, and the validation result. One successful closing cycle is not sufficient evidence of long-term correction.
Przygotuj pełne informacje o wymianie, gdy element jest poza specyfikacją
Once inspection confirms that a positioning pin, guide component, or bushing requires replacement, provide the supplier with enough information to reproduce the intended geometry rather than the worn condition.
Przygotować się:
- The approved component drawing and revision.
- The component’s function: Lokalizacja, Przewodnictwo, or final positioning.
- Pin and mating-bushing dimensions.
- Mounting and retention details.
- Required fit and tolerances.
- Materiał, Twardość, Obróbka cieplna, and surface requirements stated on the drawing.
- Ilość.
- The worn sample, when useful and available.
- Photographs or notes showing the failure pattern.
- Confirmation of whether the mating component or mounting bore will also be repaired.
- Required inspection documentation.
SunshinePro podaje, że dostarcza standardowe i rysunkowe niestandardowe rozwiązania Standardowe części formy, including guide components and dowel pins. The company also lists locating-pin guide bushings and describes inspection processes for custom components.
After the failed component and its mating conditions have been measured, the next practical step is to Przedłóż wymagania dotyczące rysunku i wymiany Do recenzji. The request should describe the verified failure and required geometry rather than asking a supplier to reproduce an unmeasured worn sample.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
