



Lista kontrolna inspekcji sworzni perforowanych dla przychodzących i rutynowych kontroli jakości
A punch pin inspection checklist should answer four questions: Is this the correct punch? Does it match the approved specification? Is it still fit for service? What action should follow the inspection?
This guide covers individual punch pins used in metal-stamping dies. Incoming QC verifies a newly supplied punch against the purchase order, rysunek, revision, oraz wymagana dokumentacja. Routine QC checks whether a punch remains serviceable after production use, Ponowne szlifowanie, a collision, or another abnormal event.
Punch pins work within a larger die system. Guides, tulejki, retainers, stripper components, Oczyszczanie, and alignment can all influence punch condition. The broader roles of these components are covered in the Przewodnik po komponentach matrycy (wnioskowane). Proszę, the focus stays on inspecting and dispositioning the punch pin itself.
No universal tolerance, inspection interval, or wear limit applies to every punch pin. Acceptance must be based on the approved drawing, purchase specification, control plan, or another documented requirement.
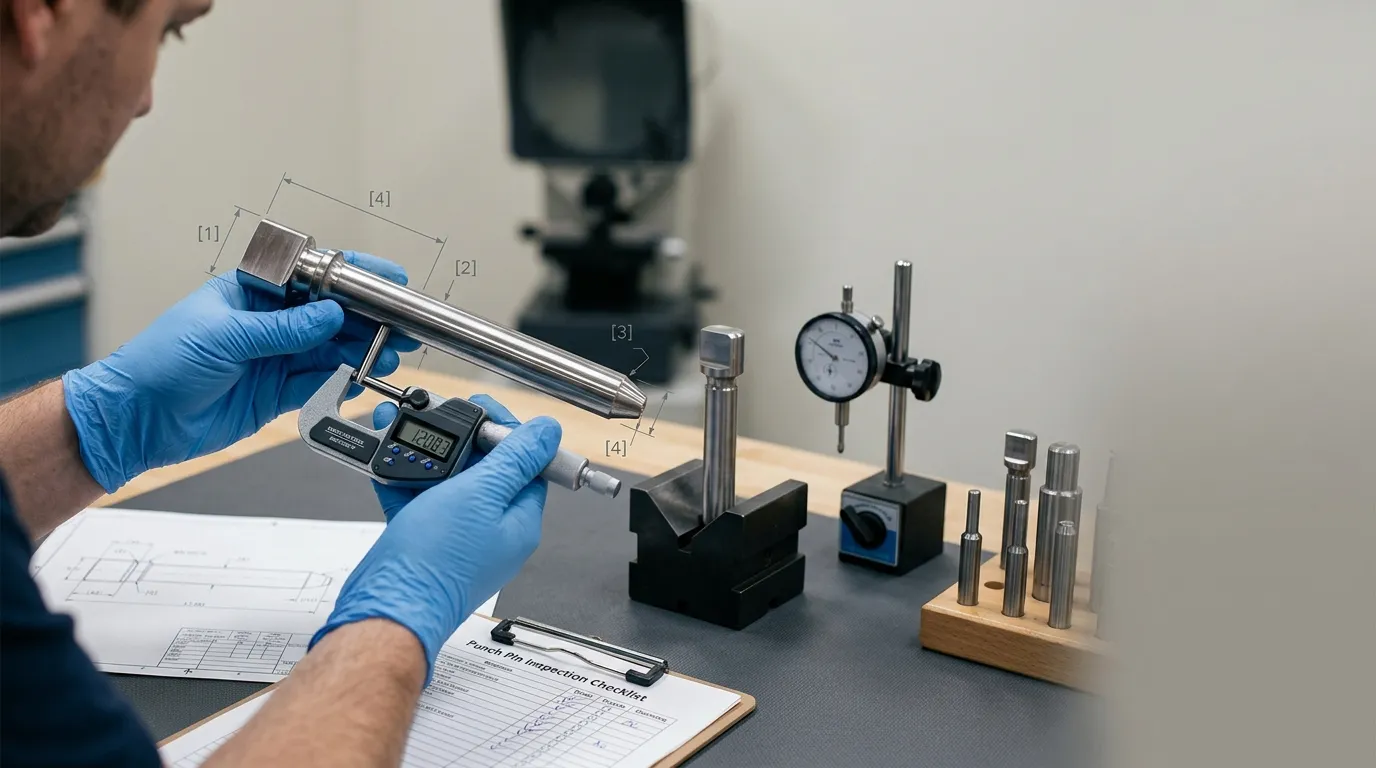
Nadchodząca kontrola jakości i rutynowa kontrola kontroli jakości Różne ryzyka
Incoming and routine inspection use many of the same instruments, but they answer different questions.
| Etap inspekcji | Główne przeznaczenie | Typowe testy | Główna decyzja |
|---|---|---|---|
| Nadchodząca kontrola jakości | Potwierdź, że dostarczony dziurkarz odpowiada zamówieniu i zatwierdzonej specyfikacji | Part identity, Poprawka rysunku, material or coating documents, visible damage, Wymiary, Geometria, inspection report | Accept, hold, return, or reject |
| Rutynowa kontrola jakości | Sprawdź, czy używany punch pozostaje bezpieczny i funkcjonalny | Zużycie krawędzi, pęknięcia, irytujące, Zmiana wymiarowa, runout, Długość robocza, Objawy produkcji, regrind history | Powrót do służby, monitor, regrind, Zamień, or investigate |
| Inspekcja po ponownym szlifowaniu | Upewnij się, że ostrzenie przywróciło krawędź, nie czyniąc innych elementów nieakceptowalnymi | Edge form, burr removal, Całkowita długość, Długość robocza, Profil, Stan powierzchni | Release, Przeróbka, lub zastąpić |
| Inspekcja po wydarzeniu | Check for hidden or visible damage after a jam, Kolizja, misfeed, or nearby breakage | Pęknięcia, bending, head damage, runout, Powierzchnie siedzące, Składniki łączące | Kwarantanna, zbadać, Naprawa, lub zastąpić |
Incoming inspection should establish a reliable baseline. Recording the punch’s as-received dimensions and condition makes later wear easier to identify.
Routine inspection compares the current punch against that baseline and any approved service limits. A punch can remain within its original manufacturing tolerance yet show an abnormal wear trend. Natomiast, a worn feature may still appear visually acceptable while no longer meeting the documented service requirement.
Prepare the Punch, Dokumenty, and Measuring Equipment
Inspection should not begin with a caliper. It should begin with the correct documents, part identity, and measurement conditions.
- Confirm the inspection stage. Record whether the punch is incoming, in routine service, newly reground, or being checked after an abnormal event.
- Obtain the approved drawing. Verify the drawing number and revision before measuring anything. An accurate measurement against an obsolete revision is still an invalid inspection result.
- Review the purchase and quality requirements. Check the purchase order, control plan, approved sample, inspection-report requirement, and any requested material, Obróbka cieplna, Twardość, or coating documentation.
- Match the punch to its records. Confirm the part number, lot or serial number, Ilość, material designation, coating designation, and any engraved identification.
- Inspect the packaging before cleaning. Record impact damage, Korozja, broken protective packaging, loose punches, or signs that sharp edges contacted each other during transport.
- Clean the punch carefully. Usuń olej, ziemia, Chipy, and transferred material without rounding the cutting edge or scratching a coated surface. Residue on a diameter or seating face can affect the measurement.
- Stabilize the part when tolerances are tight. A punch arriving from a hot production area, cold warehouse, or vehicle may need time to reach the inspection environment. Temperature differences can affect dimensional results.
- Verify the measuring equipment. Check instrument identification, calibration status, measuring range, Rozdzielczość, Stan kontaktu, and cleanliness. Confirm that any V-block, środek, Terminarz, or surface plate is also clean and suitable for the feature.
SunshinePro states that non-standard mold parts can be processed from customer drawings, while its punch-pin page lists diameter, Długość, Styl głowy, Jakość materiałowa, and coating as customizable characteristics. Those fields should therefore be treated as drawing- and order-specific requirements rather than assumed product defaults.
Rozwiązywanie sprzecznych lub brakujących specyfikacji przed pomiarem
Do not select a tolerance from memory, an old inspection sheet, or a generic catalog.
Place the punch on hold when:
- the drawing revision does not match the purchase order;
- the inspection report refers to another part or lot;
- the drawing and purchase specification contain conflicting limits;
- the material or coating designation is missing;
- the required datum or measurement method is unclear;
- an approved deviation is mentioned but not supplied.
Obtain written clarification from the responsible engineer, customer, or supplier before assigning a pass or fail result. The controlling-document hierarchy should follow the customer’s quality system or contract rather than an informal assumption.
Sprawdź każdą funkcję puncha pod kątem widocznych uszkodzeń
Visual inspection is the fastest way to find obvious defects, but it should follow a consistent feature-by-feature sequence.
Use clean lighting and suitable magnification. Rotate the punch and inspect the complete circumference rather than viewing only one side.
| Strefa inspekcyjna | Warunki do sprawdzenia | Możliwe znaczenie | Typowa kolejna akcja |
| Krawędź tnąca i końcówka | Odpryskiwanie, pęknięcia, Zaokrąglanie krawędzi, burrs, deformacja, pickup | Loss of cutting quality, przeciążenie lokalne, Wpływ, zużycie, adhesive material transfer | Miara, quarantine, regrind, lub zastąpić |
| Trzon lub korpus | Punktacja, irytujące, wear bands, Korozja, Fretting, Materiały przekazane | Poor guidance, tarcie, Niedopasowanie, lubrication problem, Nieprawidłowe dopasowanie | Czyste, measure diameter/runout, inspect mating parts |
| Głowa i ramię | Grzyby, Peening, pęknięcia, uneven seating marks, deformacja | Przeciążenie, incorrect seating, retainer problem, niewystarczające wsparcie | Przeprowadz kwarantannę i sprawdź stan aparatu zaliczkowego lub miejsca do siedzenia |
| Promienie przejścia | Pęknięcia, grinding marks, abrupt surface changes | Stężenie naprężeń, Obrażenia od grindowania, fatigue initiation | Magnify, escalate, lub zastąpić |
| Powierzchnia powlekana | Peeling, łuszczenie się, Zadrapania, Przebarwienia, Odsłonięte podłoże | Coating damage, tarcie, Wpływ, Korozja, zużycie | Record location, assess function, seek engineering review |
| Znaki identyfikacyjne | Missing or illegible part, lot, or serial information | Utrata śledzowalności lub ryzyko mieszania poprawek | Czekaj, aż tożsamość zostanie potwierdzona |
A small chip at the cutting edge is not equivalent to a superficial scratch on a non-working surface. The inspection record should state the defect location, approximate extent, and whether it affects a functional feature.
Pęknięcia, Silne odkształcenie, or a damaged retention head generally justify immediate quarantine. Galling, pickup, or one-sided scoring may require inspection of the die system as well as the punch. Detailed causes of cracking and catastrophic failure belong in the guide to Pęknięcie dziurkownika w matrycach tłoczących.
Czego inspekcja wizualna nie może potwierdzić
Visual inspection cannot reliably establish:
- exact body or tip diameter;
- overall or working length;
- prostość;
- runout, Koncentryczność, or coaxiality;
- shaped-tip profile;
- numerical surface roughness;
- Jakość materiałowa;
- heat-treatment conformity;
- Twardość;
- coating identity.
A punch may look undamaged but still be dimensionally out of tolerance. Jakość materiałowa, Twardość, and coating conformity may require traceable documentation or a specified test method.
Mierz wymiary i geometrię kontrolujących dopasowanie i funkcjonowanie
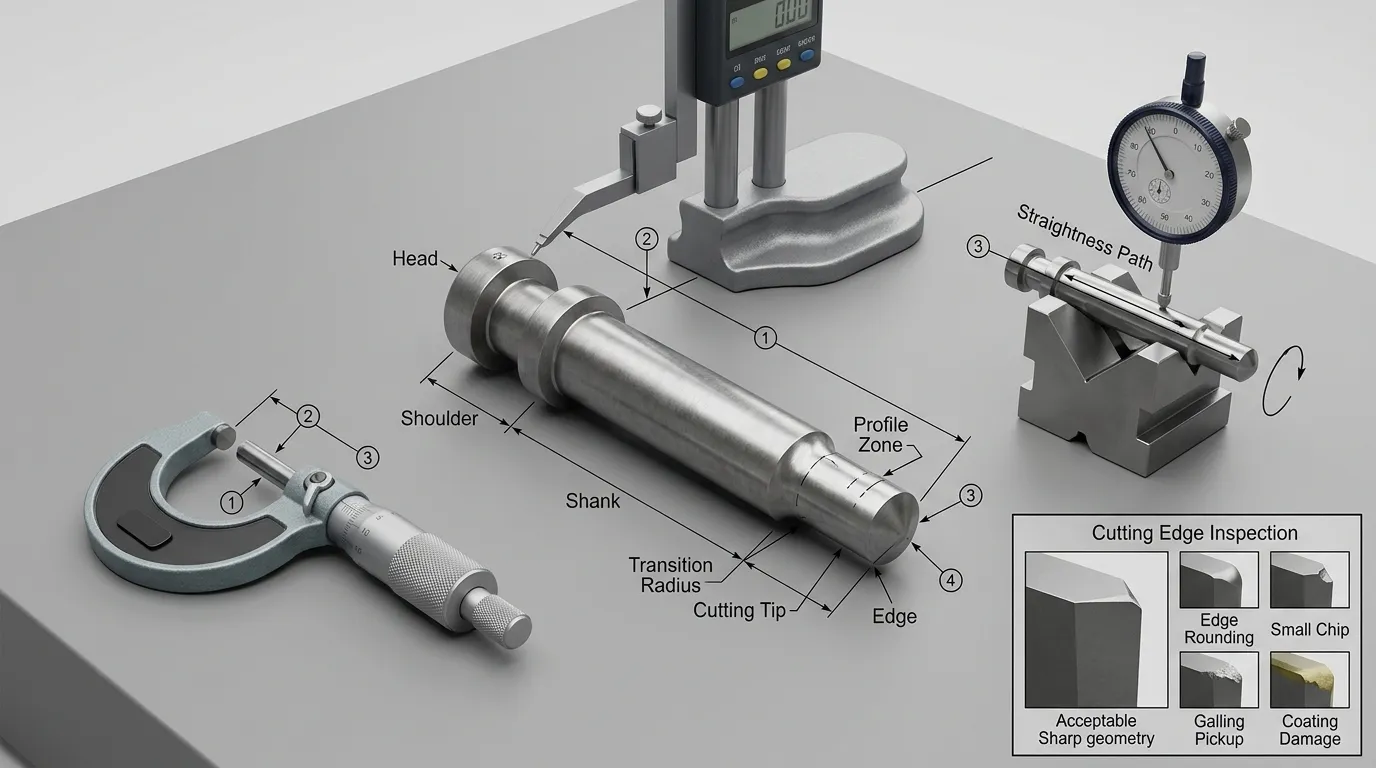
The approved drawing determines which dimensions and geometric controls must be inspected. Not every punch requires every measurement.
| Charakterystyka | Dlaczego to ma znaczenie | Możliwa metoda pomiaru | Znaczące ograniczenie | Źródło akceptacji |
| Średnica korpusu lub trzonka | Affects guidance, Dopasowanie, Utrzymanie, oraz przebieg | Outside micrometer; suitable limit gauge | Należy wziąć pod uwagę lokalizację kontaktu i stopniowe zmniejszanie | Specyfikacja rysunku lub dopasowania |
| Średnica grotu | Wpływa na rozmiar cech przebitych oraz relację między dziurkaczem a kostką | Mikrometr, specialized gauge, optical system | Małe lub delikatne końcówki mogą nie pasować do standardowych styków | Rysunek |
| Profil końcówki o kształcie | Steruje otworami nieokrągłymi lub kształtowaną geometrią | Optical comparator, vision system, CMM | Wymaga poprawnego wyrównania danych i interpretacji profilu | Rysunek z wymogiem profilu |
| Całkowita długość | Supports identification, installation, and regrind tracking | Height gauge, micrometer, komparator, dedicated fixture | Twarze siedzeń muszą być czyste i konsekwentnie odwoływane | Rysunek |
| Długość robocza lub rzut | Wpływ na pozycję operacyjną i penetrację | Height gauge, komparator, dedicated inspection fixture | Definition must match the drawing; do not borrow tablet-tooling terminology | Specyfikacja rysunku lub ustawienia |
| Średnica i grubość głowicy | Wpływa na utrzymanie i miejsce siedzące | Mikrometr, caliper for screening, komparator | Zadziorny lub przytłoczenia mogą zniekształcać kontakt | Rysunek |
| Pozycja barku | Wpływy na siedzenia i projekcję złożoną | Height gauge, komparator, CMM | Układ danych danych musi odtworzyć wymagania rysunkowe | Rysunek |
| Prostość | Wykrywa zgięcie lub odchylenie osi | Indicator with suitable support, CMM, dedicated fixture | Metoda wsparcia i wybór danych danych wpływają na wynik | Limit eksploatacji lub zatwierdzony |
| Okrągły lub całkowity wyjazd | Pokazuje zmienność obrotową względem osi odniesienia | Indicator with centers or V-block; CMM | "Runout" musi dokładnie odpowiadać kontroli rysowania | Rysunek |
| Koncentryczność lub współosiowość | Ocena zależności między osiami lub cechami | CMM lub zatwierdzona metoda specjalistyczna | Nie zastępuj prostym sprawdzeniem runout, chyba że inżynieria to zatwierdzi | Rysunek |
| Prostopadłość | Wpływa na ustawienie siedzenia lub ustawienie końcowych ścian i barków | Indicator, surface plate setup, CMM | Wymaga ważnego odniesienia danych | Rysunek |
| Chropowatość powierzchni | Can influence friction, Dopasowanie, Premiera, and galling | Tester chropowatości powierzchni | Parametr, Przerwa, Kierunek, and location must be specified | Rysunek lub specyfikacja powierzchni |
| Twardość | Może potwierdzić wymóg obróbki cieplnej | Zatwierdzony test twardości lub dokumentacja dostawcy | Test scale, Lokalizacja, Stan powierzchni, and indentation effect matter | Specyfikacja rysunku lub materiału |
Geometric terms should be interpreted according to the drawing standard in use. ISO 1101 defines geometrical tolerancing concepts in the ISO system, podczas gdy ASME Y14.5 is widely used for US-oriented GD&T drawings.
A drawing that specifies runout should not be rewritten as concentricity during inspection. These controls describe different requirements and may require different measurement strategies.
SunshinePro’s tungsten-carbide punch page lists micrometer or caliper checks, projector measurement, and roughness testing for that product category. Those published methods show the types of inspection that may be relevant, but they do not prove that every punch or every order receives the same checks.
Wybierz instrument zgodnie z tolerancją i właściwościami
Instrument choice should be based on the feature, tolerancja, Dostęp, and required measurement confidence.
| Instrument | Najlepsze zastosowanie | Główne ograniczenie |
| Mikrometr | Dostępne zewnętrzne średnice i grubości | Contact geometry may not suit small, Stożkowa, delicate, or irregular features |
| Zacisk | Identification, broad dimensions, and screening | Rozdzielczość i wpływ operatora mogą być nieodpowiednie dla ścisłych tolerancji |
| Miernik wysokości i płyta powierzchniowa | Axial dimensions, shoulder positions, and comparative height checks | Wymaga kontrolowanego siedzenia i ustawienia danych danych |
| Wskaźnik tarczowy z blokiem V-blokiem lub centrami | Runout, rotational variation, and some straightness checks | Wyniki w dużej mierze zależą od pozycji podpory i symulacji danych danych |
| Optyczny komparator lub system wizualny | Profiles, kąty, Promienie, tip shapes, and edge form | Requires alignment, magnification control, and correct profile interpretation |
| CMM | Geometria złożona i relacje oparte na danych danych | Probe access, Fiksowanie, strategy, and uncertainty must be controlled |
| Wskaźnik go/no-go | Szybka funkcjonalna weryfikacja limitu rozmiaru | Daje informacje o zaliczeniu/niezaliczeniu, ale nie pokazuje rzeczywistego odchylenia ani trendu zużycia |
| Tester chropowatości | Numeryczna weryfikacja tekstury powierzchni | Requires the correct parameter, Kierunek, Przerwa, and measurement location |
Proste limitowe wskaźniki są objęte przez ISO 1938-1. A go/no-go gauge can be efficient for repeated checks, but variable measurement is still useful when the actual size or rate of wear matters.
Surface-texture requirements should be read from the drawing rather than inferred from appearance. ISO 21920-1 covers the indication of profile surface texture in technical product documentation.
Zdecyduj, czy wynik jest akceptowalny
A measured value is not meaningful until it is compared with an approved requirement.
Possible acceptance sources include:
- the current approved drawing;
- the purchase specification;
- the control plan;
- an approved customer deviation;
- an approved sample with defined measurement criteria;
- a documented service limit;
- a validated internal wear limit.
Nominal size alone does not determine acceptance. A drawing dimension of 10 mm, na przykład, cannot be judged without its tolerance and any related geometric or surface requirements.
Use a controlled decision process:
| Warunek wyniku | Wymagana odpowiedź |
| Wyraźnie mieści się to w ramach wymogu | Zapisz wynik i przyjmij lub zwróć dziurkacz do serwisu |
| Bliski limitu lub niespójny | Verify cleanliness, Temperatura, instrument, method, Fiksowanie, datum setup, oraz powtarzalność |
| Poza wymogiem | Izoluj dziurcz i rozpocznij proces zatwierdzonej niezgodności |
| Specyfikacja jest nieobecna lub jest sprzeczna | Czekaj, aż otrzymasz pisemne wyjaśnienie |
| Powtarzające się wady po wymianie lub ponownym szlifowaniu | Zbadaj szerszy system matryc i warunki procesu |
Measurement uncertainty becomes important near a specification limit. ISO 14253-1 provides decision rules for proving conformity or nonconformity while accounting for measurement uncertainty.
In practical terms, a borderline reading should not be accepted or rejected casually. Confirm that the instrument and method are capable of resolving the requirement, then apply the organization’s documented decision rule.
Próbkowanie lub 100% inspekcja zależy od ryzyka i wymagań kontraktowych
The inspection quantity should be determined by:
- customer or contract requirements;
- characteristic criticality;
- lot size;
- supplier performance history;
- process capability;
- failure consequence;
- previous nonconformities;
- whether the result is needed for wear trending;
- the control plan.
A statement such as “100% inspected” should identify which characteristics were checked. It may mean every punch received an identification and visual check, while only selected pieces received complete dimensional inspection.
Go/no-go gauging may support rapid inspection of every piece, but it does not provide the variable data needed to evaluate size distribution or wear trends.
Stosuj rutynowe inspekcje, aby śledzić zużycie przed awarią
Routine QC should be based on risk and production history rather than one fixed interval for every punch.
Establish a baseline when the punch is first accepted, approved after setup, or returned from regrinding. Record dimensions and visible condition for the features most likely to change.
Trigger inspection when any of the following occurs:
- a planned production or maintenance interval is reached;
- the punch completes a high-risk or high-volume run;
- burr height or edge quality changes;
- stamped dimensions begin to drift;
- scratching or pickup appears on the part;
- stripping force increases;
- press load or operating sound changes;
- slug pulling or jamming occurs;
- a misfeed, Kolizja, or material double-feed occurs;
- a nearby punch chips or breaks;
- the tool is removed for maintenance;
- Smarowanie, stock material, or process settings change;
- the punch returns from regrinding.
Compare current values with the baseline and approved service limits. Trend data can reveal gradual wear before a dimension crosses a rejection limit.
Production symptoms should be treated as inspection triggers, Nie diagnozy automatyczne. Burrs may result from a worn punch, but they can also reflect die wear, Dostęp, Przebieg trasy, work-material variation, or stripper problems. The Przewodnik po formach wybicia provides broader context on die materials, Tolerancje, Dostęp, and system-level tooling considerations.
Sprawdź dziurk ponownie po ponownym szlifowaniu lub nietypowym zdarzeniu
A sharp edge does not by itself prove that a reground punch is ready for service.
Po ponownym szlifowaniu, Sprawdzone:
- cutting-edge form;
- burr-free condition;
- Całkowita długość;
- working length or projection;
- tip diameter or profile;
- surface damage or overheating;
- remaining regrind allowance, where documented;
- identification and regrind history.
After a collision, misfeed, jam, or nearby breakage, also check:
- pęknięcia;
- permanent bending;
- head or shoulder deformation;
- runout;
- Powierzchnie siedzące;
- guide and retainer contact;
- the mating die opening and surrounding components.
Do not return a punch to service solely because no visible crack is present. A collision can change alignment or runout without producing an obvious surface defect.
Zapisz wynik i przypisz kontrolowane rozwiązanie
Inspection records should identify the punch, the requirement, the method, the result, and the final decision.
Co najmniej, Rekord:
- Numer części;
- Liczba rysunków i rewizja;
- dostawca;
- purchase order;
- lot or serial number;
- material and coating designation;
- inspection stage;
- characteristic inspected;
- specification and tolerance;
- measured result;
- instrument identification;
- inspector;
- inspection date;
- disposition;
- Przypisy, photographs, or defect location where useful.
Use a controlled disposition rather than an informal “looks okay” decision.
| Znalezienie | Możliwy układ |
| Wszystkie wymagane cechy są zgodne | Przyjmij lub powróć do służby |
| Wynik jest niespójny lub bliski granicy | Czyste, stabilize, remeasure, or verify with a more capable method |
| Brakuje dokumentacji | Wstrzymaj lub poddaj kwarantannę do czasu przedstawienia dowodów |
| Naprawialne zużycie krawędzi w ramach zatwierdzonego limitu | Wyślij po ponowne szlifowanie zatwierdzone przez inżynierię |
| Crack, Poważne odpryski, permanent bending, or unsafe head damage | Zamień lub odrzuć |
| Wymiar wykracza poza wymagania | Kwarantanna i proces jako niezgodny z normami |
| Te same obrażenia powtarzają się wielokrotnie | Investigate clearance, Przebieg trasy, Wskazówki, Utrzymanie, Smarowanie, oraz warunki procesu |
Nonconforming punches should be clearly identified and physically segregated so they cannot return to production accidentally.
SunshinePro states that its quality approach includes raw-material inspection, Monitorowanie w trakcie procesu, Testy końcowe, measuring equipment, and inspection reports. Buyers should still define the required inspection characteristics and documentation for each order rather than assume that one standard report fits every punch.
Co zażądać od dostawcy sworzni do dziurkowania
A buyer should define inspection evidence before the order is released, especially for custom or critical punches.
Request the items that are relevant to the application:
- Zatwierdzony rysunek i poprawki;
- part, lot, and serial identification requirements;
- drawing-specific inspection report;
- material certificate or certificate of conformity;
- heat-treatment or hardness evidence where specified;
- coating documentation where specified;
- zatwierdzone odchylenia;
- packing and corrosion-protection requirements;
- identification of characteristics receiving 100% inspection;
- identification of characteristics inspected by sampling;
- measurement method for tight or complex tolerances;
- traceability between the punch, certificate, and inspection report.
Broad catalog statements are not a substitute for characteristic-level evidence. A supplier may state a general tolerance capability, but the buyer still needs confirmation that the required feature, Materiał, Geometria, and measurement method are suitable for the specific drawing.
SunshinePro lists tool steel, Stal szybka, Węglik, Obróbka CNC, precyzyjne szlifowanie, EDM, Obróbka próżniowa, and drawing-based customization on its punch-related pages. These published options can support an RFQ discussion, but the exact material, Proces, tolerancja, Powłoka, and inspection documentation should be confirmed for the individual part.
Podsumowanie listy kontrolnej inspekcji sworzni dziurkanej
Use this condensed sequence for incoming, routine, post-regrind, and post-event inspections:
- Identify the inspection stage.
- Confirm the part number, lot or serial number, rysunek, and revision.
- Review the purchase order, control plan, and document requirements.
- Inspect packaging and record transport damage.
- Clean the punch without damaging its edge or coating.
- Verify instrument condition, Zasięg, Rozdzielczość, and calibration status.
- Inspect the cutting edge, Podpowiedź, body, głowa, Ramię, Promienie, Powłoka, and identification.
- Measure the dimensions and geometric characteristics required by the drawing.
- Use an instrument suitable for the feature and tolerance.
- Compare results with the approved acceptance source.
- Verify borderline results and account for measurement uncertainty.
- Record the specification, result, instrument, inspector, oraz data.
- Accept, hold, quarantine, regrind, Zamień, or reject through a controlled disposition.
- Investigate the wider die system when the same damage repeatedly returns.
For a custom or replacement punch, submit the approved drawing together with the required material, Powłoka, inspekcja, and documentation needs. SunshinePro's Szpilka Punch page provides its published product context, oraz Strona kontaktowa can be used to request drawing review or clarify inspection-report requirements.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
