



Formy do dziurkowania: Rodzaje, Materiały, Tolerancje, oraz Przewodnik Zakupowy
Punching dies are precision tooling systems used for cutting, shaping, and forming sheet materials in industrial manufacturing. Buyers should compare die types, tool steel vs carbide materials, Zdolność tolerancji, clearance control, supplier machining standards, and logistics readiness before ordering. The best punching die setup depends on production volume, Twardość materiału, required accuracy, Oczekiwania dotyczące utrzymania, and supplier quality control.
Choosing the wrong die setup can increase scrap rates, shorten tool life, and delay production schedules. Buyers also face pressure to balance cost, Precyzja, and lead time, especially when sourcing custom tooling from overseas suppliers. This guide explains how punching dies work, które materiały działają najlepiej, how tolerances affect quality, oraz co sprawdzić przed złożeniem zamówienia.
What are punching dies and how do they work?
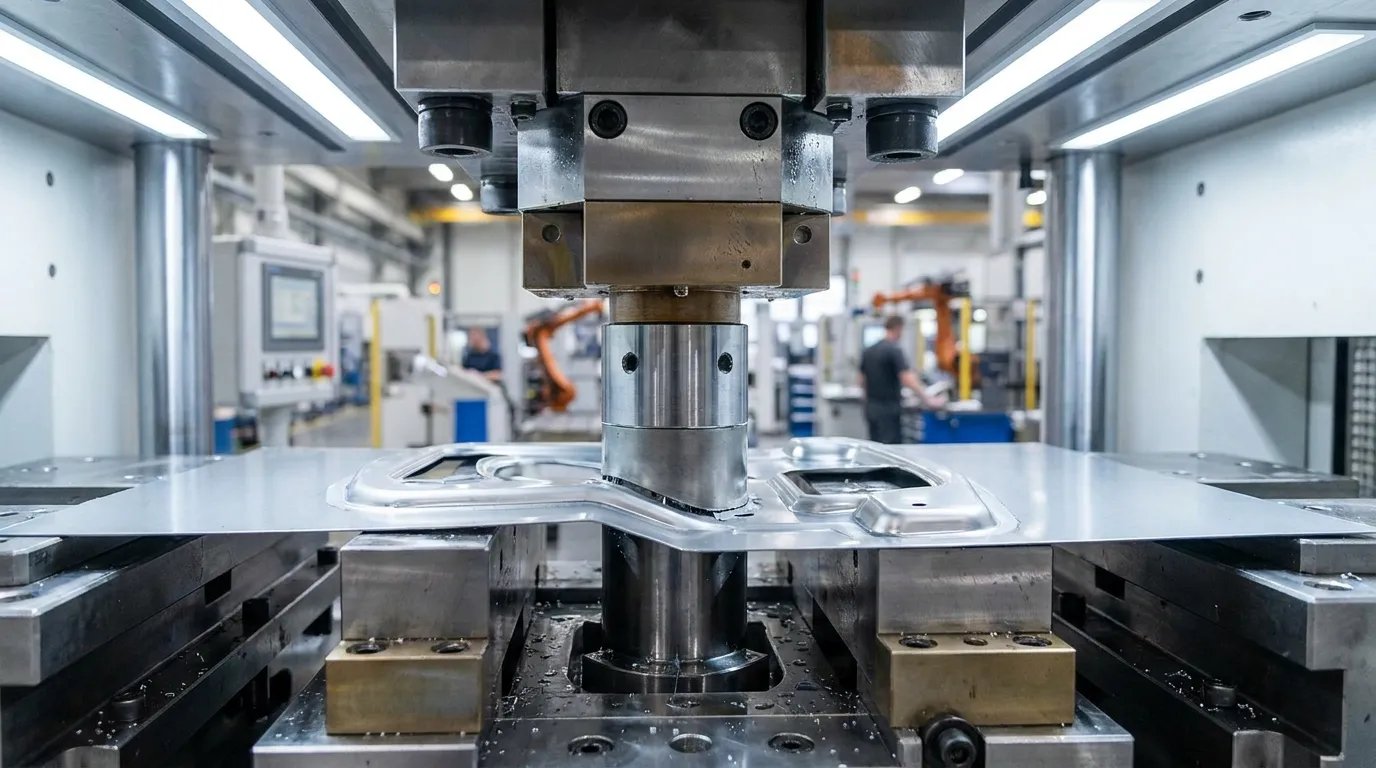
Punching dies are tooling systems used to cut, Kształt, or form material through controlled force and precision alignment. The punch applies pressure while the die receives and shapes the material, allowing consistent high-volume production in stamping and forming operations.
A punching die system includes two core components: the punch and the die. The punch presses into the material, while the die supports the material and controls the final shape. This process is common in sheet metal stamping, Produkcja części samochodowych, Produkcja elektroniki, and appliance components.
The accuracy of the tooling directly affects edge quality, burr formation, and repeatability. Even small alignment issues can create uneven cuts or excessive wear. That’s why manufacturers focus heavily on machining precision, Obróbka cieplna, and clearance control during production.
Kupujący, którzy potrzebują szerszego przeglądu systemów narzędzi przemysłowych, mogą to zapoznać się Przewodnik po komponentach formy wraz z podstawami narzędzi wyjaśnionymi w Podstawy komponentów matrycy.
Terminologia branżowa dotycząca dziurkaczy i matryc jest jasno wyjaśniona przez Przewodnik terminologiczny MISUMI do dziurkania i matrycy.
Which types of punching dies are used in manufacturing?
Progressive dies support high-volume automated production, while compound dies combine multiple cutting operations in one stroke. The best choice depends on production speed, Złożoność, material thickness, i wymagało precyzji.
Different punching die designs are built for different manufacturing goals. A low-volume fabrication shop may prioritize lower tooling cost and easier maintenance. A high-speed automotive supplier usually focuses on cycle time, Spójność, oraz odporność na zużycie.
| Typ | Najlepsze zastosowanie | Główna zaleta | Ograniczenia |
|---|---|---|---|
| Progressive Die | Produkcja wielkomasowa | Szybkie automatyczne przetwarzanie | Wyższa złożoność narzędzi |
| Forma złożona | Wielokrotne operacje cięcia | Wysoka precyzja w jednym ruchu | Mniej elastyczne do formowania złożonego |
| Kostka do wybaczania | Cięcie płaskich części | Czysta produkcja blanków | Ograniczona zdolność formowania |
| Formowanie matrycy | Wyginanie i kształtowanie | Uchwyty tworzyły komponenty | Więcej różnorodności ustawień |
Formy progresywne vs złożone do dziurkania
Progressive dies move material through several stations in sequence. Each station performs a separate operation, which improves production speed for large manufacturing runs. These dies are common in automotive and electronics manufacturing.
Compound dies perform multiple cutting operations at the same station during one press stroke. They’re often used when part accuracy matters more than production speed. Według Referencja złożonej matrycy MISUMI, compound tooling structures are commonly paired with hardened tool steels such as SKD11.
For buyers comparing broader tooling categories, Systemy narzędziowe provides additional manufacturing context.
What materials are best for punching dies?
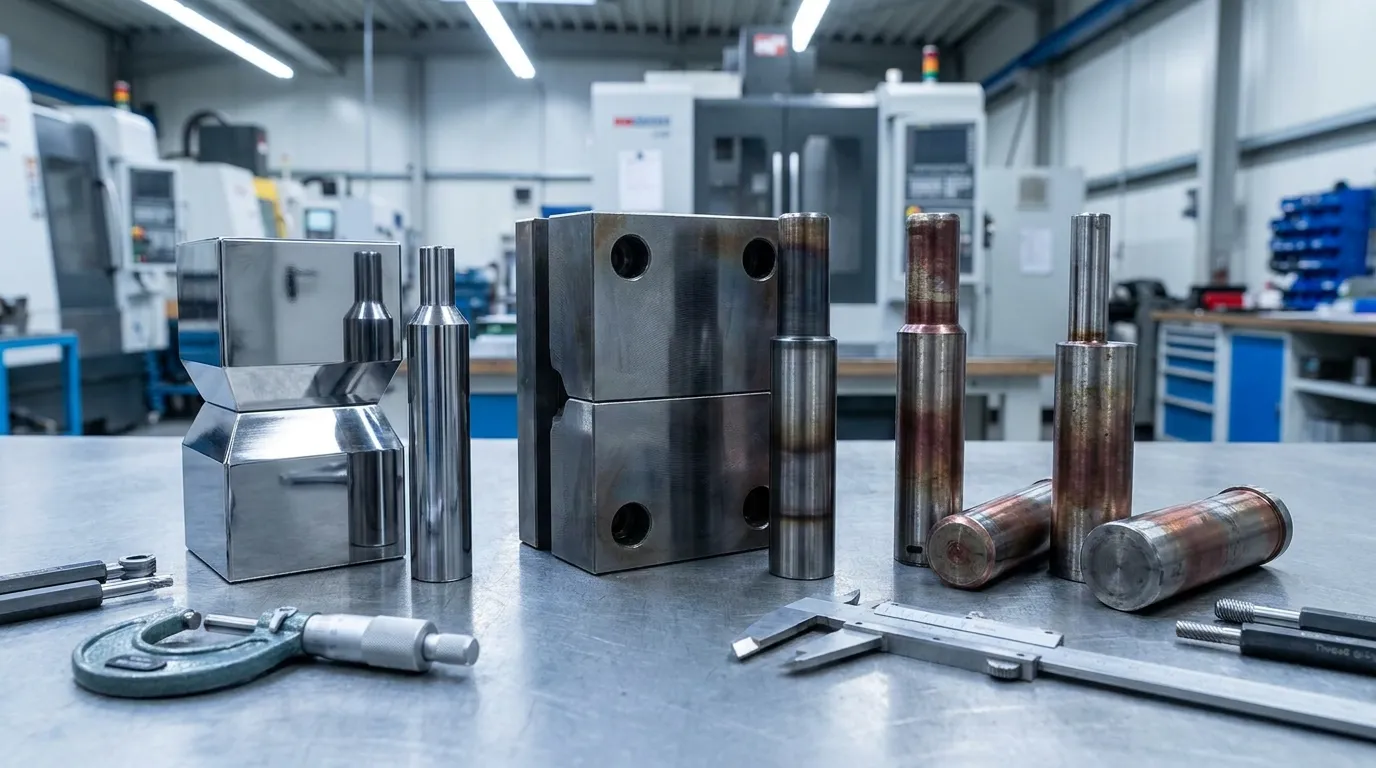
Tool steel punching dies balance durability and cost for many industrial applications, while carbide dies offer superior wear resistance for high-volume production. Material choice should match production cycles, sheet material hardness, oraz oczekiwania dotyczące utrzymania.
Tool material affects wear resistance, sharpening frequency, edge quality, and overall operating cost. Buyers should match material selection to actual production conditions instead of assuming the hardest material is always the best choice.
Carbide punching dies are not always the best option. They last longer in high-volume production, but tool steel is often easier and cheaper to maintain for shorter production runs or moderate workloads.
Tabela wyboru materiału matrycy dziurkowej
| Materiał | Odporność na zużycie | Poziom kosztów | Najlepsza produkcja | Częstotliwość konserwacji |
|---|---|---|---|---|
| D2 Tool Steel | Średnio-wysokie | Medium | Średnie serie | Umiarkowany |
| SKD11 | Wysoko | Średnio-wysokie | Precyzyjne tłoczenie | Umiarkowany |
| Węglik | Bardzo wysoki | Wysoko | Produkcja wielkomasowa | Low |
| Stal szybkotnąca | Medium | Medium | Ogólne zastosowanie przemysłowe | Umiarkowany |
A factory producing thin stainless steel brackets for automotive use may benefit from carbide tooling because downtime costs are high. W przeciwieństwie do tego, a smaller fabrication company producing limited batches may save money with tool steel dies that are easier to sharpen and replace.
Gdy węglik jest wart wyższego kosztu
Carbide becomes more practical when production volumes are high and materials are abrasive. It performs well with stainless steel, electrical steel, and other harder materials that increase wear rates.
Extremely tight tolerance claims are not automatically better. Over-specifying tolerances can raise tooling costs without improving production quality. Buyers should request tolerances that match the actual application and production environment.
Producenci porównujący materiały i komponenty narzędzi również mogą oceniać Materiały precyzyjne do narzędzi for additional component references.
Why do punch and die tolerances matter?
Punch and die tolerances directly affect cut quality, burr formation, tool wear, oraz spójność produkcji. Proper clearance helps maintain cleaner edges and longer tooling life while reducing scrap and maintenance costs.
Tolerance control determines how accurately the punch and die interact during production. Poor clearance settings can create rough edges, excessive burrs, or premature chipping. Z czasem, these issues increase scrap rates and maintenance costs.
Punch and die clearance refers to the gap between the cutting edges during operation. Według Przewodnik po poświadczeniach MISUMI, proper clearance improves cutting performance and extends tooling life.
What is punch and die clearance?
Clearance settings vary based on material thickness and hardness. Thin aluminum sheets need different clearance than thick stainless steel plates. Buyers should confirm that suppliers understand the target material before approving production drawings.
A practical example is burr reduction in thin sheet production. One manufacturer reduced secondary finishing work after adjusting clearance for thinner stainless steel stock. Cleaner edges reduced polishing time and improved consistency across production batches.
Lista kontrolna tolerancji i jakości
- Potwierdź grubość materiału przed zdefiniowaniem przerytu
- Dopasuj poziomy tolerancji do rzeczywistych potrzeb aplikacji
- Weryfikacja możliwości obróbki EDM i CNC
- Zproś raporty inspekcyjne dla wymiarów krytycznych
- Przegląd procedur ostrzenia i konserwacji
Maintenance planning also matters because worn tooling can slowly change clearance values over time. Buyers sourcing long-term replacement components can review Części narzędziowe zamienne for ongoing tooling support.
How do you choose the right punching die supplier?
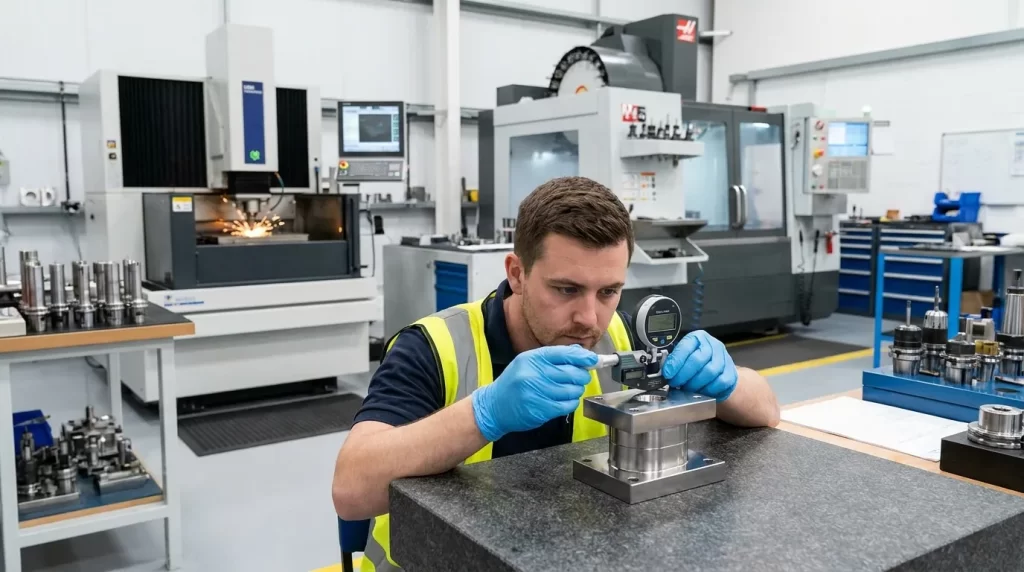
A reliable punching die supplier should provide verified material specifications, machining capabilities, tolerance controls, and quality inspection procedures. Buyers should also confirm lead times, production capacity, and experience with similar applications.
Supplier selection affects more than price. Weak machining standards or inconsistent inspection procedures can increase scrap, Czas wolny, and replacement costs long after delivery.
The cheapest overseas punching die supplier can create higher long-term costs if documentation, clearance control, or quality inspection standards are inconsistent. Buyers should compare supplier capability, not just quotation pricing.
Lista kontrolna oceny dostawcy formacji do dziurkowania
| Obszar oceny | Co potwierdzić |
|---|---|
| Możliwości CNC | Wydajność obróbki precyzyjnej |
| Możliwości przewodowego EDM | Precyzyjna dokładność cięcia |
| Certyfikacja materiałów | Zweryfikowane gatunki stalowe lub węglikowe |
| Dokumentacja QC | Raporty inspekcyjne i tolerancje |
| Niezawodność w czasie realizacji | Realistyczne harmonogramowanie produkcji |
| Wsparcie eksportowe | Koordynacja pakowania i wysyłki |
A strong supplier should also understand the buyer’s industry requirements. An automotive stamping supplier may need different tolerances than an appliance manufacturer or electronics producer.
If you’re evaluating broader tooling manufacturing experience, Doświadczenie w produkcji matryc provides additional context about industrial die production capabilities.
What should buyers include in a punching die RFQ?
A detailed RFQ helps suppliers quote accurately and reduces production misunderstandings. Missing technical details often lead to delayed revisions, incorrect tolerances, or tooling redesigns after production begins.
An effective punching die RFQ should include:
- Rysunki CAD lub pliki 3D
- Specyfikacja materiałów
- Wymagane tolerancje
- Szacunki wielkości produkcji
- Oczekiwania dotyczące wykończenia powierzchni
- Docelowy czas realizacji
- Informacje o maszynie prasowej, jeśli mają znaczenie
A common sourcing mistake happens when buyers provide drawings without tolerance details. One supplier may quote for standard machining tolerance, while another assumes ultra-precision requirements. That difference can change pricing and lead time significantly.
For projects involving custom tooling configurations, Rozwiązania dla niestandardowych matryc can help buyers compare available options before requesting quotations.
How can buyers reduce customs and shipping delays for punching dies?
Nieprawidłowe kody HS, Niekompletne faktury, and missing compliance documents are common causes of customs delays for industrial tooling shipments. Buyers can reduce delays by confirming classification accuracy and documentation requirements before shipment.
International tooling shipments often move through multiple customs checks before delivery. Even accurate tooling production can become a problem if shipping paperwork is incomplete or incorrectly classified.
Według Kodowa referencja HS FreightAmigo, industrial tooling classifications must match the actual product category and intended use. Documentation errors are also identified as a common cause of customs delays in Przewodnik po opóźnieniach celnych EximAgent.
Lista kontrolna zapobiegania opóźnieniom w odprawie celnej
- Zweryfikować klasyfikację kodu HS przed wysyłką
- Używaj szczegółowych opisów produktów na fakturach
- Dołącz dokumentację kraju pochodzenia
- Potwierdzaj, czy opakowanie zgadza się z dokumentami wysyłkowymi
- Przegląd wymagań importowych z partnerami frachtowymi
- Prowadź rejestry komunikacji z dostawcami i celnikami
One imported tooling shipment experienced delays because the invoice described the product only as “metal tooling.” Customs officers requested additional classification details, which delayed delivery and production scheduling. A more detailed invoice could have prevented the issue.
What maintenance practices extend punching die lifespan?
Regular maintenance reduces wear, poprawia spójność, and protects tooling accuracy over time. Even high-quality dies lose performance when sharpening schedules and inspections are ignored.
A preventive maintenance approach usually costs less than replacing damaged tooling unexpectedly. Buyers should confirm that maintenance procedures are realistic for their production environment before selecting tooling materials.
Lista kontrolna konserwacji matryc do dziurkowania
- Regularnie sprawdzaj krawędzie tnące
- Monitorowanie powstawania zadziarów podczas produkcji
- Przestrzegaj zaplanowanych interwałów ostrzenia
- Store tooling in dry, protected conditions
- Sprawdź geometrię i prześwit podczas konserwacji
- Wymień zużyte elementy prowadnic niezwłocznie
A small production facility using tool steel dies may sharpen tooling more often but spend less on replacement costs overall. High-volume manufacturers often accept higher carbide tooling costs because fewer production stoppages offset the investment.
Producenci planujący długoterminowe harmonogramy konserwacji mogą to zbadać Części serwisowe narzędzi for replacement component support.
Poprawne wykonanie kolejnego kroku
The best punching dies are the ones that match your production reality. Material hardness, Produkcja, Wymagania tolerancyjne, and supplier capability all affect long-term performance and operating cost.
Before placing an order, confirm machining standards, inspection procedures, material certification, and shipping documentation requirements. A lower upfront price does not always mean lower production cost over time.
If your team is comparing broader tooling systems or manufacturing applications, reviewing an Zastosowania w formach wtryskowych resource can also help connect punching die selection with larger production planning decisions.
Najczęściej zadawane pytania
Jaka jest różnica między dziurkaczem a kostką?
A punch applies force while the die shapes and supports the material. Both components work together to create accurate cuts, holes, or formed shapes during stamping and punching operations.
What materials are commonly used for punching dies?
Tool steel and carbide are the most common punching die materials. Tool steel balances durability and cost, while carbide performs better in high-volume or high-wear manufacturing environments.
What is punch and die clearance?
Punch and die clearance is the controlled gap between cutting components. Proper clearance improves edge quality, reduces burr formation, and helps extend tooling lifespan during production.
Which punching die type is best for high-volume production?
Progressive dies are widely used for high-volume production. They perform multiple operations in sequence, which improves speed, Spójność, and automation efficiency in large manufacturing runs.
What causes punching dies to wear out quickly?
Incorrect clearance and poor maintenance are major causes of punching die wear. Excessive production load, improper material selection, and delayed sharpening schedules can also shorten tooling lifespan.
What documents help avoid customs delays for industrial tooling?
Accurate shipping and classification documents help reduce customs delays. Commercial invoices, HS codes, and origin documentation should all match the actual tooling being imported.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
