



Narzędzia B vs narzędzia D: Wymiary, Pojemność, oraz Kompatybilność
B tooling and D tooling are dimensional families of tablet press punches and dies. B tooling has a smaller punch barrel and die envelope, which can allow more stations on a given turret. D tooling is physically larger and commonly accommodates a larger tablet envelope and different dwell configurations.
Neither is universally better. The correct choice depends on the installed press and turret, Geometria tablicy, Zachowanie formułowania, required dwell and compression conditions, Standard narzędzi, and production target. For broader context on B, D, BB, and DB configurations, Zobacz Rodzaje narzędzi do prasy do tabletów.
“Capacity” also needs a clear definition. In a B tooling vs D tooling comparison, it can refer to:
- The size of tablet the tooling can accommodate;
- the number of stations and potential production output;
- the compression and dwell conditions available to form an acceptable tablet.
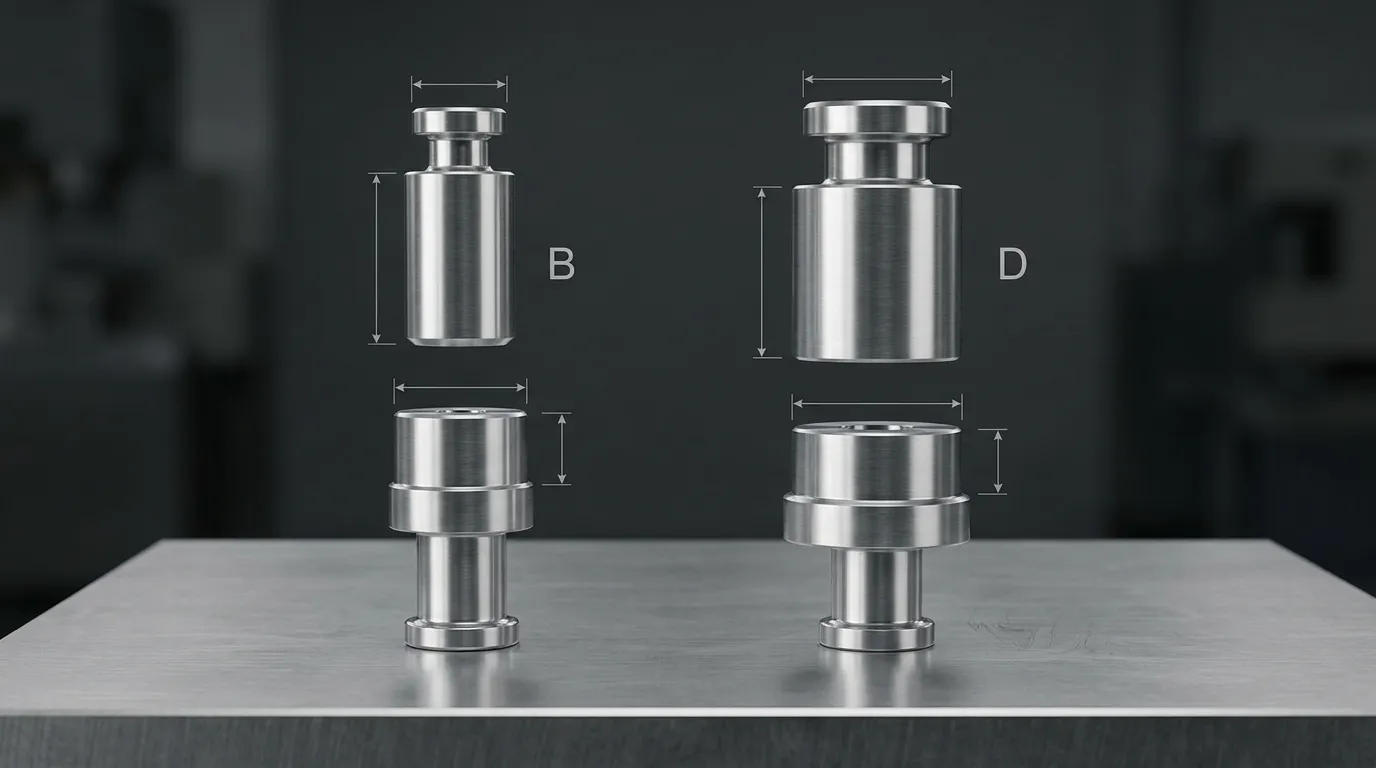
Narzędzia B i D w porównaniu na pierwszy rzut oka
| Kryterium porównawcze | Narzędzia B | Narzędzia D |
|---|---|---|
| Nominalna średnica lufy dziurkaczowej | Około 19 mm | Około 25,35 mm |
| Nominalna średnica zewnętrzna głowicy dziurkaczowej | Około 25,27 mm | Około 31,6 mm |
| Średnica zewnętrzna zwykłej matrycy | Około 30,16 mm | Około 38,10 mm |
| Wspólna wysokość matrycy | Około 22,22 mm | Około 23,81 mm |
| Wspólny maksymalny referencyjny okrągły tablet | Do około 16 mm | Do około 25 mm |
| Tendencja do gęstości stacji wieży | Wyżej, where the turret is designed for B tooling | Niższy niż porównywalna wieżyczka B, ponieważ każda stacja potrzebuje więcej miejsca |
| Tendencja do zatrzymywania się | Depends on head form, Geometria prasy, and speed | Often associated with a larger head-flat or longer dwell opportunity, but not universally |
| Typowy kierunek selekcji | Mniejsza obudowa tabletu lub większa gęstość stacji | Większa obłona tabletu lub proces wymagający innej konfiguracji głowicy i trybu zamieszkania |
| Bezpośrednia wymiana | Nie | Nie |
These are common reference dimensions, not a complete purchase specification. ISO 18084 defines principal punch-and-die dimensions, Tolerancje, Charakterystyka, and interchangeability-related measures. A KORSCH technical paper also lists 19 mm and 25 mm nominal punch barrels, with 30.16 mm and 38.10 mm die diameters for B and D configurations respectively. The approved tooling and turret drawings must control the final order. Tepha 4Itech Standardy 4Itech 4
Różnice wymiarowe wpływające na dopasowanie narzędzi
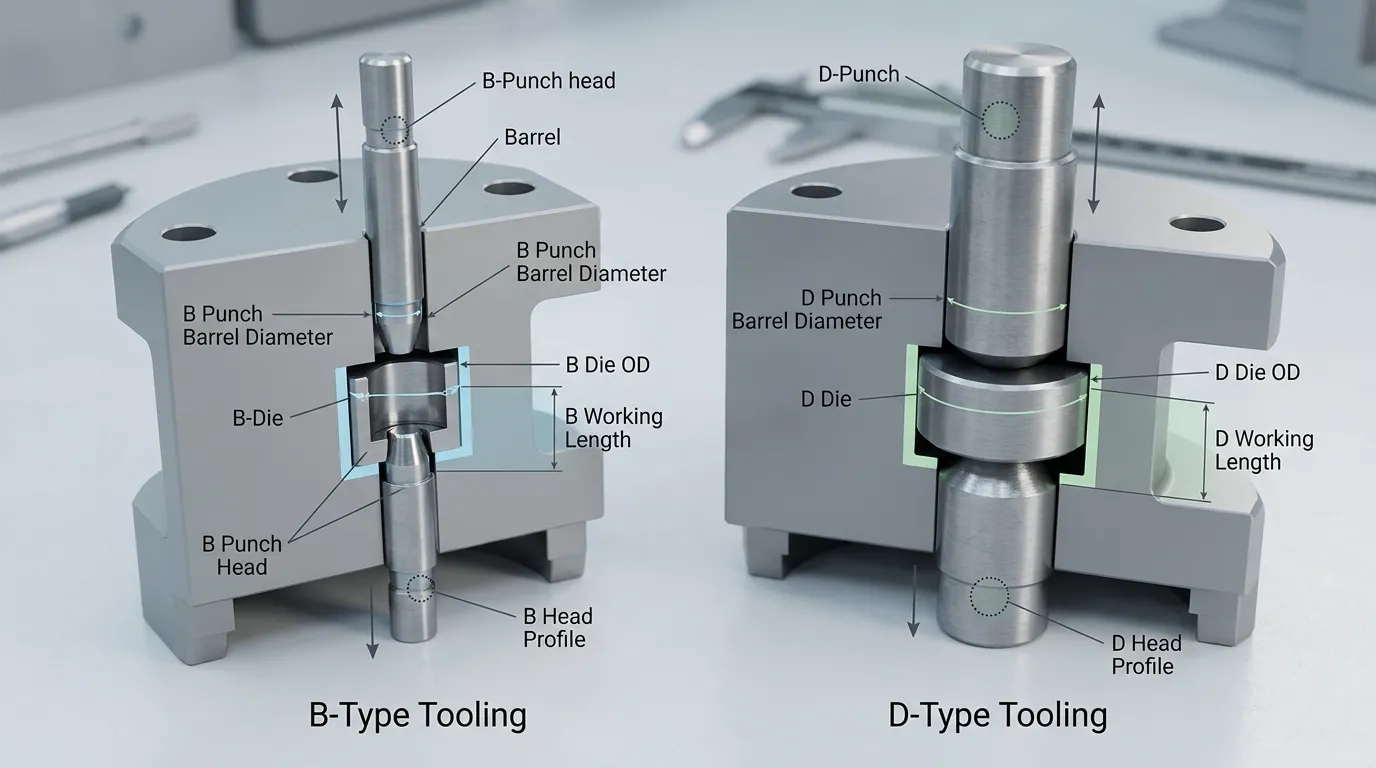
The visible size difference between B and D tooling is not merely a capacity preference. It determines whether the components can physically run in a particular turret.
A punch barrel travels through a precisely sized punch guide. A B punch with a nominal barrel near 19 mm cannot simply replace a D punch designed for a guide near 25.35 mm. The same restriction applies to dies: a common B die outside diameter is approximately 30.16 mm, while a common D die is approximately 38.10 mm. The turret die pockets and retention system must match those dimensions. Standardy Itech 1
Punch-head geometry also matters. The head contacts the tablet press cams and compression rollers, so its diameter, Grubość, Promień, płaskie, and under-head geometry influence how the punch travels through the compression cycle. Two punches can share a B or D designation and still be incompatible because they follow different standards or machine-specific designs.
Wymiary dziurkania i wykroj, które muszą się zgadzać
A supplier normally needs more than the words “B tooling” or “D tooling.” The critical dimensions and features include:
- Górna- and lower-punch barrel diameter;
- punch-head outside diameter and profile;
- Górna- oraz całkowita długość o niższym uderzeniu;
- Długość robocza;
- punch-tip dimensions and cup depth;
- die outside diameter and height;
- Wymiary wywiertów matryc;
- die groove, Zwężanie, or retention features;
- anti-turn key location and angle;
- tablet press turret rotation.
Working length is especially important because variation within a tooling set can affect the final tablet thickness and consistency. Całkowita długość, barrel diameter, die OD, The Bore, and head form are also treated as critical inspection dimensions in established tooling-management guidance. I Holland Ltd
Dlaczego nominalna etykieta B lub D nie gwarantuje wymienności
B and D describe tooling-size families. Nie mają, samodzielnie, confirm the complete standard.
Euro/ISO and TSM configurations may differ in punch-head form, head flat, Grubość głowicy, under-head cam angle, nominal overall length, oraz kluczowanie. Those differences can restrict interchangeability even when both tools are described as B tooling or both as D tooling. Shaped and multi-tip upper punches also require the correct anti-turn key position for the turret’s rotation and tablet take-off arrangement. I Holland Ltd
Co oznacza "pojemność" w porównaniu B-kontra-D
Tooling capacity should be evaluated in three separate categories. A family that offers more tablet-size capacity does not automatically provide more production capacity, and a larger tool does not establish a universal safe compression-force rating.
Pojemność wielkości tabletu
D tooling provides a larger physical envelope for the punch tip and die bore. A common industry reference is approximately 25 mm for a round tablet under D tooling and approximately 16 mm under B tooling. These figures are useful for preliminary screening, but they are not universal design limits. KORSCH 1
The supplier must also consider:
- Major and minor tablet dimensions;
- round or shaped profile;
- Głębokość kubka;
- edge land and web thickness;
- score-line geometry;
- tłoczenie;
- tablet thickness and target weight;
- punch-tip strength;
- clearance between the tip and die bore.
A shaped, Zdobyte, embossed, or multilayer tablet does not inherently require D tooling. Those features depend on tablet design, punch-tip geometry, Kluczowanie, machine capability, and mechanical loading. The B-or-D decision concerns the available tooling envelope and press configuration, not whether the tablet face is simple or complex.
Moc produkcyjna i gęstość stacji wieżyczek
Because B tooling uses a smaller barrel and die envelope, a turret of a given pitch-circle size can often accommodate more B stations than D stations. More stations can increase theoretical output when the press runs at the same speed.
For a single-tip, single-sided press, the basic relationship is:
Teoretyczne tabliczki na godzinę = prędkość wieżyczki w obrotach na minutę × liczba stacji × 60
For multi-tip tooling, multiply the result by the number of tablet tips at each station. KORSCH uses this relationship in its technical discussion of turret selection and multi-tip production. KORSCH
That does not mean B tooling guarantees higher real production. Actual validated output also depends on:
- Maximum sustainable turret speed;
- formulation flow and die filling;
- compression dwell requirements;
- Wydajność zasilająca;
- tablet weight-control capability;
- ejection and take-off behaviour;
- Stan narzędzi;
- rejection and inspection requirements;
- single-tip or multi-tip configuration.
A difficult-to-compress formulation may require slower operation. W takim przypadku, the station-count advantage can be partly or completely offset by the lower sustainable speed.
Siła ściskania i zdolność do zatrzymania
Dwell time is the period during which the punch tips remain at or near the minimum separation under compression. It is influenced by punch-head geometry, head-flat size, Geometria rolki ściskającej, turret pitch-circle velocity, and press speed.
D tooling is often associated with a larger head geometry and longer dwell opportunity, but the relationship is not absolute. Both B and D tools can use modified or extended head flats, and the exact result depends on the selected standard and press.
A peer-reviewed study comparing B and D tooling found that head-flat diameter and tooling type affected tablet mechanical properties, but the results also changed with formulation composition and compression force. The study therefore supports a formulation-dependent decision—not the claim that D tooling always produces stronger tablets. Badania nad narzędziami B/D oraz geometrią głowicy dziurkaczowej reported interactions among tooling type, dwell, siły, Wytrzymałość na rozciąganie, Zdrobnienie, and capping behaviour. ResearchGate+2Taylor & Francis Online+2
Natoli’s technical guidance similarly explains that increasing the punch-head flat can lengthen dwell at the same turret speed for both TSM-B and TSM-D tools. Formulation strain-rate sensitivity can determine whether that additional dwell improves production performance. Natoli Engineering
A safe maximum force cannot be selected from the B or D label alone. It also depends on the press rating, punch-tip area and shape, tool material, Obróbka cieplna, Konstrukcja głowicy, Stan narzędzia, Formułowanie, and approved engineering calculations.
Kompatybilność wymaga czegoś więcej niż wyboru B lub D
A correct tooling order must satisfy several compatibility layers:
- Tooling family: B or D;
- Standard narzędzi: EU/ISO, TSM, or another machine-specific specification;
- Geometria wieży: Prowadnice dziurkaczy, die pockets, station layout, oraz utrzymanie;
- Geometria dziurkarki: Forma głowy, Długości, Długość robocza, oraz kluczowanie;
- Geometria tablicy: Podpowiedź, Puchar, Partytura, tłoczenie, Ziemia, and die bore;
- process requirements: fill depth, siły, dwell, Wyrzucenie, and output.
Rodzina narzędzi i standard narzędzi to różne decyzje
B tooling is not synonymous with TSM tooling, and D tooling is not synonymous with European tooling. Both B and D families may be configured under TSM or EU/ISO conventions.
The standard adds dimensional details beyond the barrel and die envelope. Differences in overall length, Forma głowy, kąt pod głową, and keying can prevent a tool from running correctly in another press. For a dedicated treatment of that second compatibility layer, Zobacz Standardy narzędzi do tabletów EU vs TSM. I Holland Ltd
Szczegóły prasy i wieżyczki do weryfikacji
Before approving either family, potwierdź:
- Tablet press manufacturer and model;
- turret model, rysunek, or identification number;
- number of turret stations;
- B or D punch-guide size;
- die-pocket diameter, Wysokość, and retention design;
- Górna- and lower-punch overall lengths;
- tooling working length;
- punch-head profile and under-head geometry;
- Standard narzędzi;
- key location and key angle;
- clockwise or anticlockwise turret rotation;
- existing tooling drawing or physical reference sample.
A machine advertised as supporting several tooling families may use exchangeable turrets or another purpose-designed arrangement. That does not make ordinary B and D components interchangeable within one fixed turret.
Jak wybrać między narzędziami B a D
The existing tablet press and turret should be the first selection constraint. If the machine already uses a fixed B or D turret, changing the tooling family may require a replacement turret or more extensive machine engineering.
| Wymagania | Narzędzia B mogą być lepszym punktem wyjścia | Narzędzia D mogą być lepszym punktem wyjścia |
|---|---|---|
| Zainstalowany sprzęt | Tłoczka i wieża są zaprojektowane z myślą o narzędziach B | Tłoczka i rewolwer są zaprojektowane do zastosowań D |
| Geometria tablicy | Tablet wygodnie mieści się w zweryfikowanym ofercie narzędzia B | Tablet wymaga większej obudówki zweryfikowanego narzędzia D-tool |
| Priorytet produkcji | Większa gęstość stacji jest cenna | Wymagany wynik można osiągnąć przy dostępnej liczbie stacji D |
| Zachowanie formułowania | Akceptowalna jakość tabletu jest osiągana w dostępnym miejscu zamieszkania | Formuła korzysta z wybranej konfiguracji głowicy D i układu zawszedniowego |
| Wymóg kompresji | Obliczania siły i wytrzymałości końcówki są akceptowalne dla proponowanego narzędzia B | Proposed tablet and process require a larger tool envelope, subject to engineering verification |
| Status zgodności | B family, Standard, Długości, die, and keying are confirmed | D family, Standard, Długości, die, and keying are confirmed |
Narzędzia B są zazwyczaj lepszym punktem wyjścia, gdy
Consider B tooling when the press already has a compatible B turret, the tablet fits within its verified design envelope, and higher station density offers a useful production advantage. The formulation must still achieve the required tablet properties at the press speed and dwell available.
Narzędzia D są zazwyczaj lepszym punktem wyjścia, gdy
Consider D tooling when the press has a compatible D turret, the tablet requires a larger tip and die envelope, or the selected head geometry provides a more suitable compression window. The process must still meet its output target with the available station count and operating speed.
Zatrzymaj się i sprawdź przed wyborem któregokolwiek z nich
Do not choose from a generic size chart alone when:
- The tooling standard is unknown;
- the turret drawing is unavailable;
- the tablet is close to the assumed size limit;
- unusually high force or long dwell is required;
- shaped or multi-tip tooling needs precise key orientation;
- a replacement tool must match an existing set;
- a B-to-D or D-to-B conversion is being considered;
- the press contains proprietary or modified tooling geometry.
Typowe nieporozumienia dotyczące narzędzi B-kontra-D
| Nieporozumienie | Dokładniejsza interpretacja |
|---|---|
| D tooling is European tooling. | D is a tooling-size family. EU/ISO and TSM are separate standards layers. |
| B tooling always produces more tablets. | It can allow more stations, but real output also depends on speed, dwell, Karmienie, Formułowanie, tips per punch, oraz wymagania walidacyjne. |
| D tooling always handles more force. | Safe force depends on the press, head and tip geometry, tool material, tablet area, Formułowanie, and engineering calculations. |
| Only D tooling can produce shaped, Zdobyte, embossed, or multilayer tablets. | These features depend on the punch-tip design, Kluczowanie, Geometria tablicy, and machine capability. |
| Any B tool fits any B press. | Całkowita długość, Forma głowy, kąt pod głową, die details, Kluczowanie, and machine-specific geometry may differ. |
| The published maximum tablet diameter is a guaranteed limit. | It is a preliminary reference. The proposed design still needs mechanical and press-specific review. |
| Changing punches and dies converts a B press to D. | A different turret or machine configuration is normally required because punch guides and die pockets are different. |
Co uwzględnić w RFQ dotyczącym narzędzi B lub D
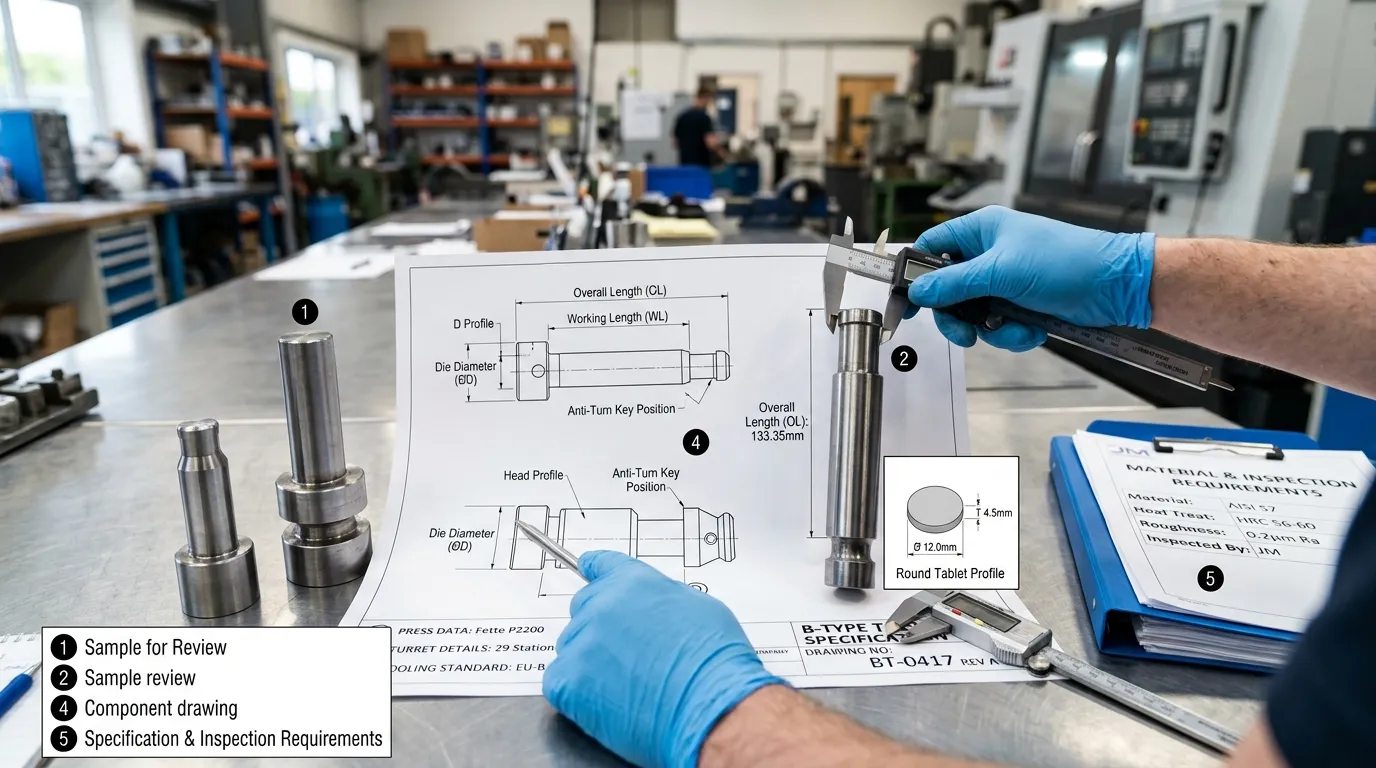
A useful tooling enquiry should contain enough information for dimensional and process review. Zawiera:
- Tablet press manufacturer and model;
- turret designation and station count;
- required B or D family;
- EU/ISO, TSM, or machine-specific standard;
- Górna- oraz rysunki o niższej grubości;
- die drawing;
- overall and working lengths;
- punch-head and under-head geometry;
- die OD, Wysokość, Otwor, groove, oraz utrzymanie;
- anti-turn key location and turret rotation;
- tablet drawing with all major dimensions;
- Puchar, Partytura, tłoczenie, Ziemia, and tolerance details;
- tablet weight and thickness targets;
- formulation concerns such as abrasion, Korozja, or sticking;
- required tool material, Obróbka cieplna, lub powłoka;
- dimensional inspection and material-documentation requirements;
- an existing sample when an approved drawing is unavailable.
SunshinePro's Narzędzia prasy do tabletów page states that it supplies tablet press punches and dies, Lista stali szybkiej, Obróbka CNC, Obróbka cieplna, and customization from drawings or samples, and says material inspection reports can be provided. These verified statements support a drawing-led enquiry, but the required B or D family, Standard, Wymiary, Materiał, and tolerance scope should be confirmed for the specific order. SunShinePro
Zasada ostatecznego wyboru: Match the Tooling to the Press, Tablet, oraz proces
Choose B or D tooling by working in this order:
- Confirm the installed press, Wieża, oraz standard narzędzi.
- Verify that the tablet geometry fits the available tooling envelope.
- Check the formulation’s dwell and compression requirements.
- evaluate output using the actual station count and sustainable press speed.
- Control the final order with approved tooling and tablet drawings.
For a custom or replacement requirement, prepare the press data, turret details, Rysunki, Standard, key orientation, and existing sample where applicable. Wtedy skontaktuj się z SunshinePro for a specification and manufacturing review rather than relying on the B or D designation alone.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
