



Die Components Guide: Uderzenia, Piny, Tuleje, and Wear Parts
TL;DR
Die components are the working parts inside a stamping die that control cutting, Przebieg trasy, guiding, stripping, oraz odporność na zużycie. Common die components include punches, die pins, Punkty przewodnika, tulejki, wear plates, and stripper systems. Choosing the right materials, Tolerancje, and replacement strategy helps reduce downtime, improve stamping accuracy, and extend tool life in high-volume production environments.
Stamping dies depend on precision. A worn punch, loose bushing, or misaligned guide post can quickly affect part quality and production speed. This guide explains the most common die components, Co robi każdy z nich, which parts wear out fastest, and how to avoid common failure problems in real production environments.
What are die components and why do they matter in stamping dies?
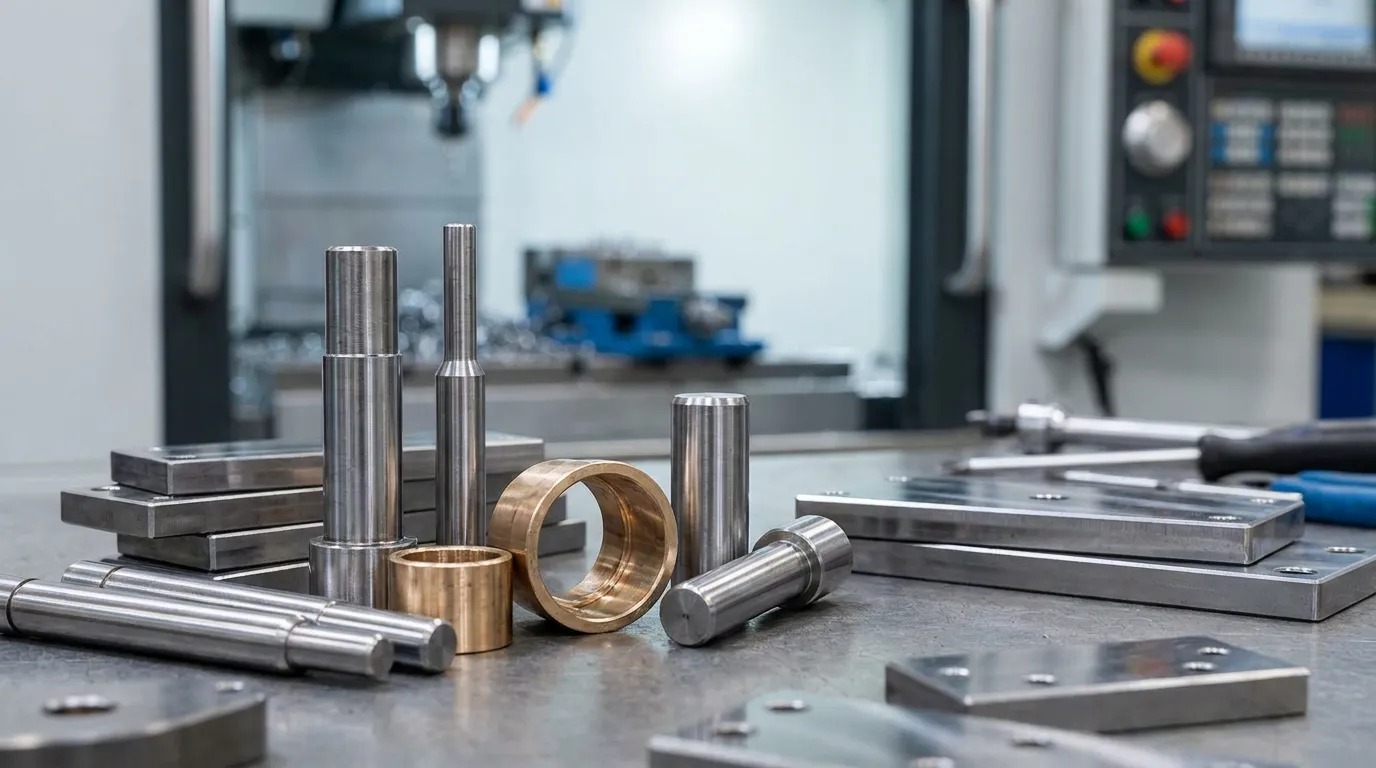
Die components are the functional parts inside a stamping die that control cutting, Przebieg trasy, guiding, oraz odporność na zużycie. Uderzenia, Punkty przewodnika, tulejki, and wear plates work together to maintain precision and repeatability during production.
Every stamping die relies on several interacting parts. Punches shape or cut the material, guide systems maintain alignment, and wear components protect the tooling from friction and repeated impact. If one component drifts out of tolerance, the entire die can lose accuracy.
Manufacturers often group these parts into standard tooling elements and custom-machined elements. Many shops use standardized replacement hardware for faster maintenance cycles. Companies that specialize in Elementy precyzyjnej formy typically focus on maintaining tight tolerances and repeatable fit across high-volume production runs.
For a broader look at tooling systems and mold architecture, the Kompletny przewodnik po komponentach formy covers how these systems work together across different manufacturing applications.
| Składnik | Główna funkcja | Typowe ryzyko zużycia |
|---|---|---|
| Uderzenia | Materiał tnijny lub formowany | Zużycie krawędzi, odpryskiwanie |
| Punkty przewodnika | Utrzymanie wyrównania | Punktacja nawierzchni |
| Tuleje | Zmniejszenie tarcia i ruch prowadnicy | Zużycie prześwity |
| Płyty zużycia | Chronić powierzchnie styku | Uszkodzenia spowodowane tarciem |
| Płytki znikające | Usuń materiał z dziurkacza | Zmęczenie sprężynowe |
Odniesienia branżowe z Fabrykator show that alignment and wear management are among the most important factors in long-term die performance.
Which die components wear out most often?
Uderzenia, Tuleje prowadzące, wear plates, and stripper components usually wear out first because they experience repeated friction, Wpływ, and alignment stress. Monitoring these parts early helps prevent expensive die damage and unplanned downtime.
Punch tips face the highest impact load in many stamping operations. Z czasem, edges round off or chip, especially when working with abrasive materials or poor lubrication. Bushings and guide elements also wear gradually as the die cycles through repeated motion.
Wear problems rarely stay isolated. A loose guide bushing can increase punch side loading, which then accelerates punch wear and damages surrounding surfaces. Shops that ignore early wear signs often end up replacing multiple components instead of one.
Tabela Priorytetów Zużycia Komponentów Rdzenia
| Składnik | Główna przyczyna zużycia | Typowy objaw niepowodzenia | Częstotliwość inspekcji | Priorytet zastępstwa |
|---|---|---|---|---|
| Końcówki do dziurków | Powtarzający się wpływ | Zadziorny na tłoczonych krawędziach | Codziennie | Wysoko |
| Tuleje prowadzące | Tarcie i niewyrównanie | Luźne wyrównanie matrycy | Tygodniowo | Wysoko |
| Płyty zużycia | Tarcie kontaktowe powierzchniowe | Punktacja lub galing | Tygodniowo | Medium |
| Sprężyny stripperowe | Zmęczenie kompresyjne | Niepełne rozbieranie | Miesięcznik | Medium |
| Punkty przewodnika | Słabe smarowanie | Drgania lub dryf | Miesięcznik | Medium |
A progressive die line running automotive brackets may replace guide bushings after dimensional drift appears during inspection. Replacing the bushings during scheduled maintenance can prevent a multi-hour production stop later in the week.
For replacement inventory and wear-related tooling support, many manufacturers keep dedicated Części formy zamienne available to reduce downtime.
Dodatkowe wskazówki dotyczące zużycia od U-NEED Precision highlights how friction and poor alignment often accelerate wear across several connected parts at the same time.
What does each major die component do?
Different die components perform different mechanical jobs. Some parts cut material, while others guide movement, Siła pochłaniająca, or protect the die from wear. Understanding each role makes troubleshooting much easier during production problems.
Dziurkacze i sworznie
Punches are the cutting or forming elements inside the die. They push through sheet material to create holes, shapes, or bends. Die pins may help position or align material depending on the tooling design.
Repeated regrinding can extend punch life, but it is not always the safest long-term option. Regrinding changes punch geometry over time, which may increase alignment risk in high-precision tooling.
High-volume production lines often prefer standardized punches because replacements are easier to source quickly. Shops looking for consistent replacement tolerances commonly use Precyzyjne części matryc to simplify maintenance planning.
Słupki drogowe i tuleje
Guide posts and bushings control alignment between upper and lower die sections. Even minor clearance changes can affect cutting accuracy and punch wear.
Bushings reduce friction during repeated die movement. Proper lubrication and hardness matching are important because excessive friction quickly damages both surfaces.
Płyty zużycia i systemy zmywaczy
Wear plates protect high-contact surfaces from repeated sliding movement. Stripper systems remove material from the punch after each cycle and help maintain stable part release.
Harder materials are not always better for these components. Extremely hard tooling may resist wear longer, but it can also become brittle and chip under high-impact loads.
Materiały referencyjne z Moeller Punch oraz Fabrykator shows how specialty wear and alignment components improve consistency in demanding stamping applications.
How do guide posts and bushings affect die accuracy?
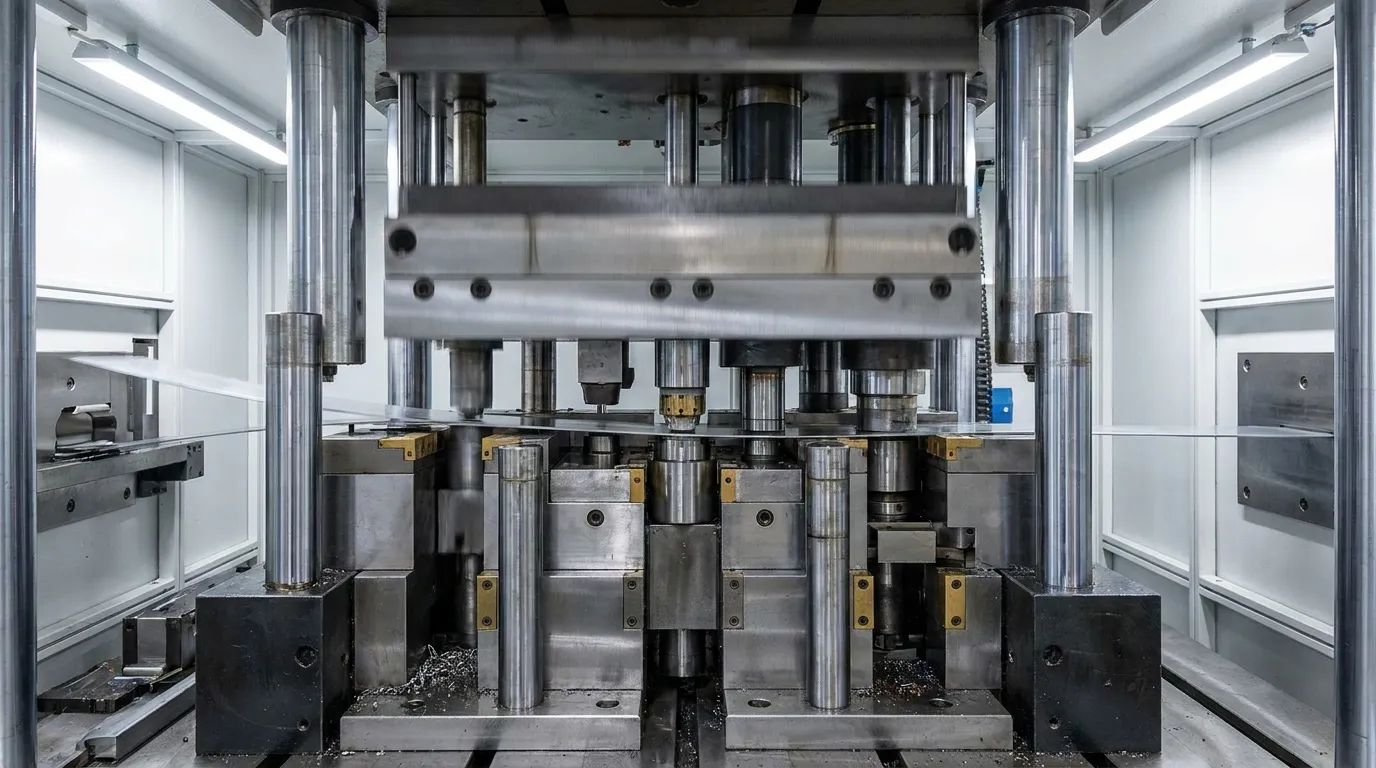
Guide posts and bushings keep upper and lower die sections aligned during every press stroke. Even small alignment errors can increase punch wear, damage cutting edges, and reduce dimensional consistency in stamped parts.
Alignment systems are often overlooked until problems appear on finished parts. In reality, guide components affect almost every stage of die movement. If bushings wear unevenly, the punch may enter the die block slightly off-center, increasing friction and edge stress.
A medical device tooling project may require custom guide pins to maintain micron-level consistency across thin metal parts. W takich przypadkach, standard components may not provide enough positional control for stable production.
Typowe objawy problemów z wyrównaniem
- Nierówne zużycie ciosów
- Zwiększone drgania
- Formacja żarna
- Zarysowania na tłoczonych częściach
- Przedwczesne odpryskiwanie krawędzi
Standardized alignment hardware is still the best option for many production lines because replacement is simpler and faster. Shops sourcing Tuleje prowadzące often prioritize repeatable fit and quick inventory access during maintenance shutdowns.
Odniesienia do układu komponentów z Technologia Ready show how guide systems support die stability during repetitive press cycles.
Standard vs custom die components: which should you use?
Standard die components reduce lead time and simplify replacement, while custom components solve unique geometry, Dostęp, or production challenges. The best choice depends on tooling complexity, Wymagania tolerancyjne, oraz częstotliwość wymiany.
Standard components work well for many production environments because they are widely available and easier to replace quickly. They also simplify inventory management across multiple tooling systems.
Custom components become more important when the die includes unusual shapes, ścisłe tolerancje, or difficult forming conditions. Automotive and medical tooling often require custom-machined alignment or wear solutions.
Standardowa a niestandardowa tabela decyzyjna komponentów
| Czynnik | Komponenty standardowe | Komponenty niestandardowe |
|---|---|---|
| Czas realizacji | Szybciej | Dłuższy |
| Prędkość zastępcza | Łatwiej | Wolniej |
| Koszty | Dolny front | Wyższy start |
| Elastyczność tolerancji | Limitowane | Wyższa precyzja |
| Najlepszy przypadek użycia | Prace o dużej objętości | Specjalistyczne narzędzia |
Standard components are not always the best choice. They work well when tooling geometry follows common industry dimensions, but custom parts are safer when alignment tolerances are unusually tight or clearance requirements vary between stations.
Producenci porównujący opcje zaopatrzenia często przeglądają Standardowe komponenty matrycy alongside custom tooling requirements before finalizing a maintenance strategy.
What causes die component failure and misalignment?
Most die component failures come from misalignment, słabe smarowanie, excessive side loading, or incorrect material hardness. Small alignment problems often accelerate wear across punches, tulejki, and cutting surfaces at the same time.
Many failures begin with small setup issues that gradually worsen during production. A punch operating under side load may still function temporarily, but repeated stress can crack edges or damage bushings over time.
Poor lubrication is another common issue. Friction increases heat buildup, which damages contact surfaces and accelerates scoring. In high-cycle stamping operations, lubrication consistency matters just as much as component hardness.
Typowe przyczyny uszkodzenia matrycy
- Zużyte tuleje
- Nieprawidłowe rozmowy matrycy
- Boczny ładunek
- Zanieczyszczenie gruzem
- Nieprawidłowa obróbka cieplna
- Słabe smarowanie
- Nadmierne szlifowanie przy wybijaniu
An automotive stamping line may lose two hours of production because of progressive alignment drift caused by worn bushings. Replacing those bushings during preventive maintenance would usually cost far less than emergency downtime and scrap material losses.
A separate issue appears when tooling is hardened too aggressively. Harder materials resist wear longer, but brittle punches are more likely to chip during impact-heavy operations. Material balance matters more than maximum hardness alone.
Producenci poszukujący wysokiej trwałości zamienników często porównują różne Części matryc odporne na zużycie based on operating load and production volume.
Dodatkowe obserwacje konserwacyjne z U-NEED Precision show how lubrication and alignment problems frequently appear together in failed tooling systems.
How should die components be maintained and replaced?
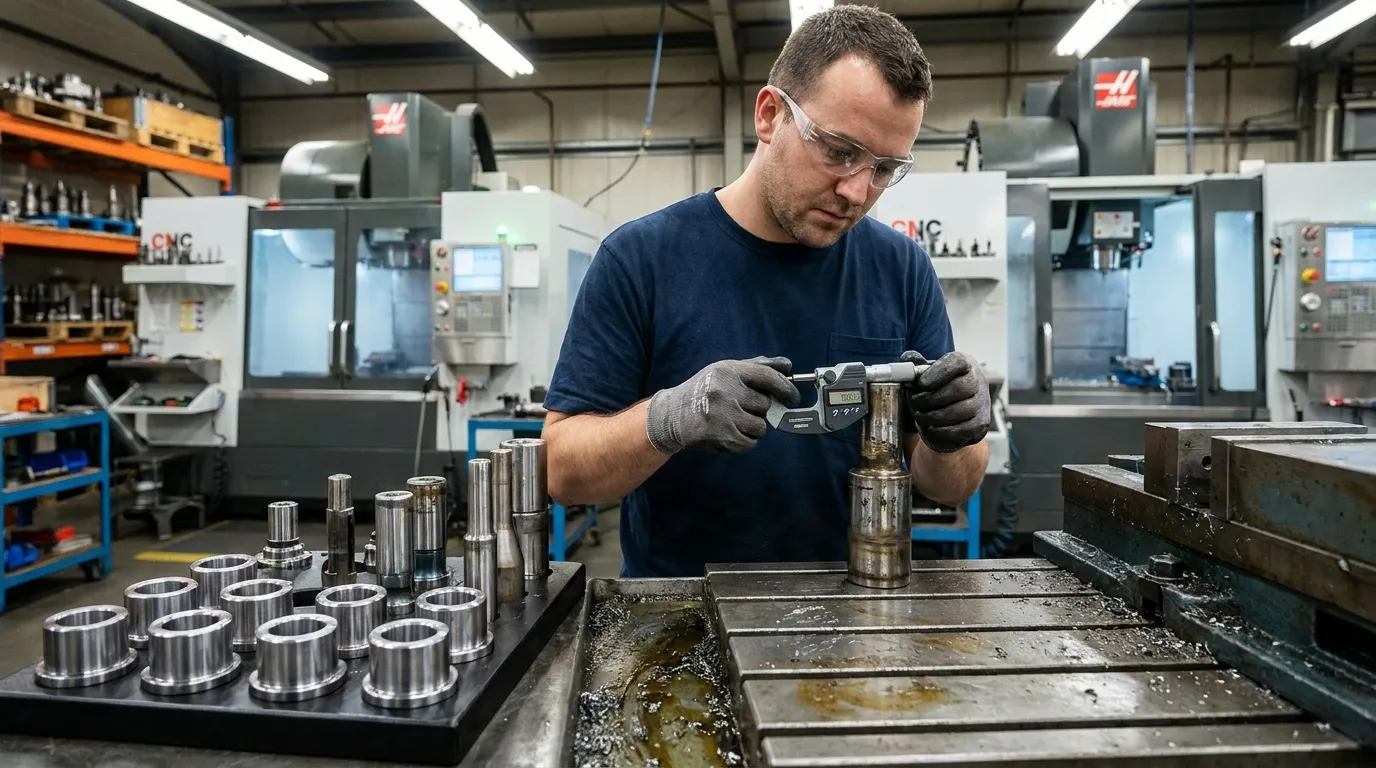
Regular inspection and planned replacement cycles help prevent major die failures. Most shops monitor punches, tulejki, and wear surfaces closely because these parts usually fail before larger structural sections.
Maintenance schedules depend on material type, Tempo produkcji, and tooling complexity. High-volume progressive dies often require more frequent punch inspections than lower-cycle forming operations.
Podstawowa lista kontrolna konserwacji
- Inspect punch edges for chipping or burr formation.
- Check bushings for excess clearance or scoring.
- Verify lubrication consistency across moving surfaces.
- Monitor stripper spring compression and return movement.
- Remove debris buildup inside die cavities.
- Measure alignment drift during scheduled maintenance.
- Replace high-wear components before adjacent damage appears.
A simple downtime calculation shows why preventive replacement matters. If a press line loses two hours of production during emergency punch failure, labor and production losses can easily exceed the cost of scheduled replacement parts.
Warsztaty zarządzające systemami narzędzi na zamówienie często polegają na Komponenty narzędzi na zamówienie to maintain consistent tolerances after repeated maintenance cycles.
For readers who want a broader understanding of tooling systems beyond stamping dies, the Przewodnik po formowaniu wtryskowym tworzyw sztucznych explains how different mold structures support manufacturing accuracy across industries.
Poprawne wykonanie kolejnego kroku
Choosing the right die components is about more than replacing worn parts. Stabilność wyrównania, Wybór materiałów, Smarowanie, and maintenance timing all affect production quality and tool life. A well-maintained stamping die usually costs less over time because it reduces scrap, Czas wolny, and emergency repairs.
If your tooling setup includes frequent punch wear, alignment drift, or inconsistent part quality, start by reviewing the wear-priority components first. Standard replacement parts work well in many cases, but complex tooling often benefits from custom-machined solutions built around tighter tolerances and specific production loads.
Najczęściej zadawane pytania
What are the main components of a stamping die?
The main stamping die components include punches, die blocks, Punkty przewodnika, tulejki, stripper plates, wear plates, and springs. Each part supports cutting accuracy, Przebieg trasy, or material control during the stamping cycle.
What is the difference between a punch and a die?
A punch is the male component that pushes through material, while the die is the matching female section that receives the punch. Razem, they create the required cut or formed shape.
Which die components wear out fastest?
Końcówki do dziurków, Tuleje prowadzące, wear plates, and stripper components usually wear out first because they face repeated friction and impact. Regular inspection helps prevent expensive die damage and unexpected downtime.
What causes die misalignment?
Die misalignment is commonly caused by worn bushings, poor setup, Boczny ładunek, debris buildup, or damaged guide components. Even small alignment errors can reduce part accuracy and increase tool wear.
Are standard die components better than custom parts?
Standard components are usually faster and cheaper to replace, while custom parts are better for unusual tooling designs or tight tolerances. The best choice depends on production requirements and maintenance strategy.
How often should die components be replaced?
Czas wymiany zależy od ilości produkcji, Rodzaj materiału, lubrication quality, and tooling setup. High-wear parts should be inspected regularly and replaced before they damage nearby tooling surfaces.
Udostępnij:



Napisane przez Sunshine
W Sunshine, Jesteśmy profesjonalnym producentem i dostawcą komponentów do precyzyjnych form, oferując szeroką gamę produktów do tłoczenia i formowania wtryskowego. Naszym głównym celem są formy do dziurkania, Sworznie wyrzutowe i tuleje, oraz słupy i tuleje. Dzięki zaawansowanej obróbki CNC, Ścisła kontrola jakości, oraz silne możliwości produkcyjne, Zapewniamy niezawodność, Części o wysokiej precyzji, wraz ze standardowymi komponentami dostępnymi na stanie, zapewniającymi szybkie i efektywne globalne dostawy.
WIADOMOŚCI
UZYSKAJ USŁUGĘ
Z wysokiej jakości częściami dostosowanymi do każdego budżetu oraz przyjaznym personelem przeszkolonym, by Twoja wizyta była poinformowana i bezproblemowa.
